



Blogs
Workholding
Product Selection
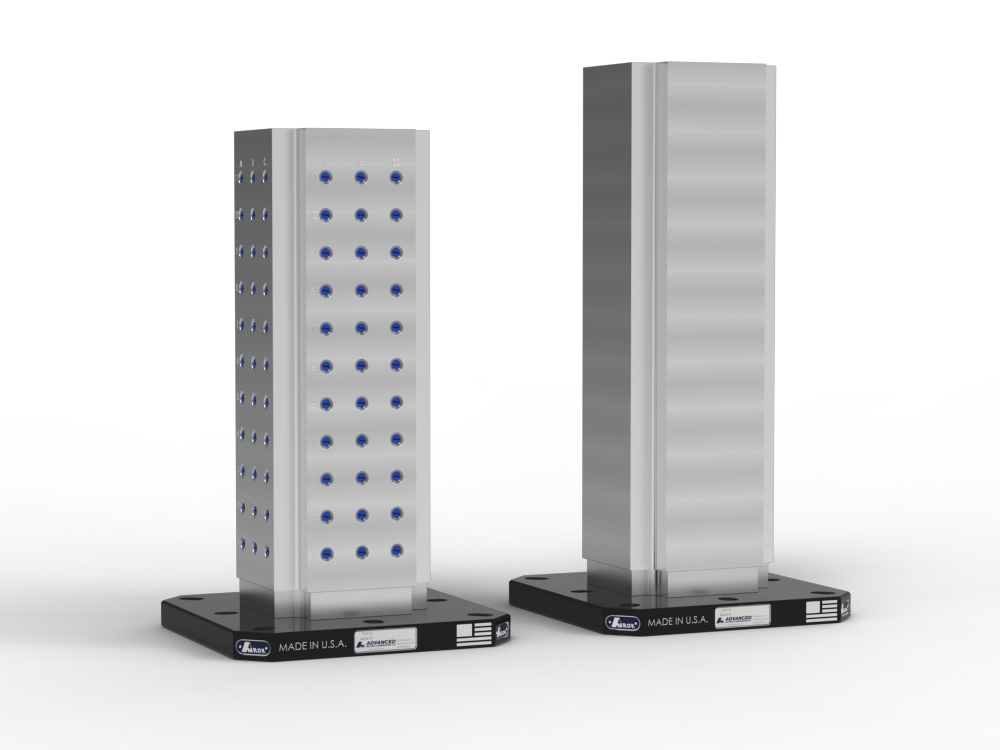
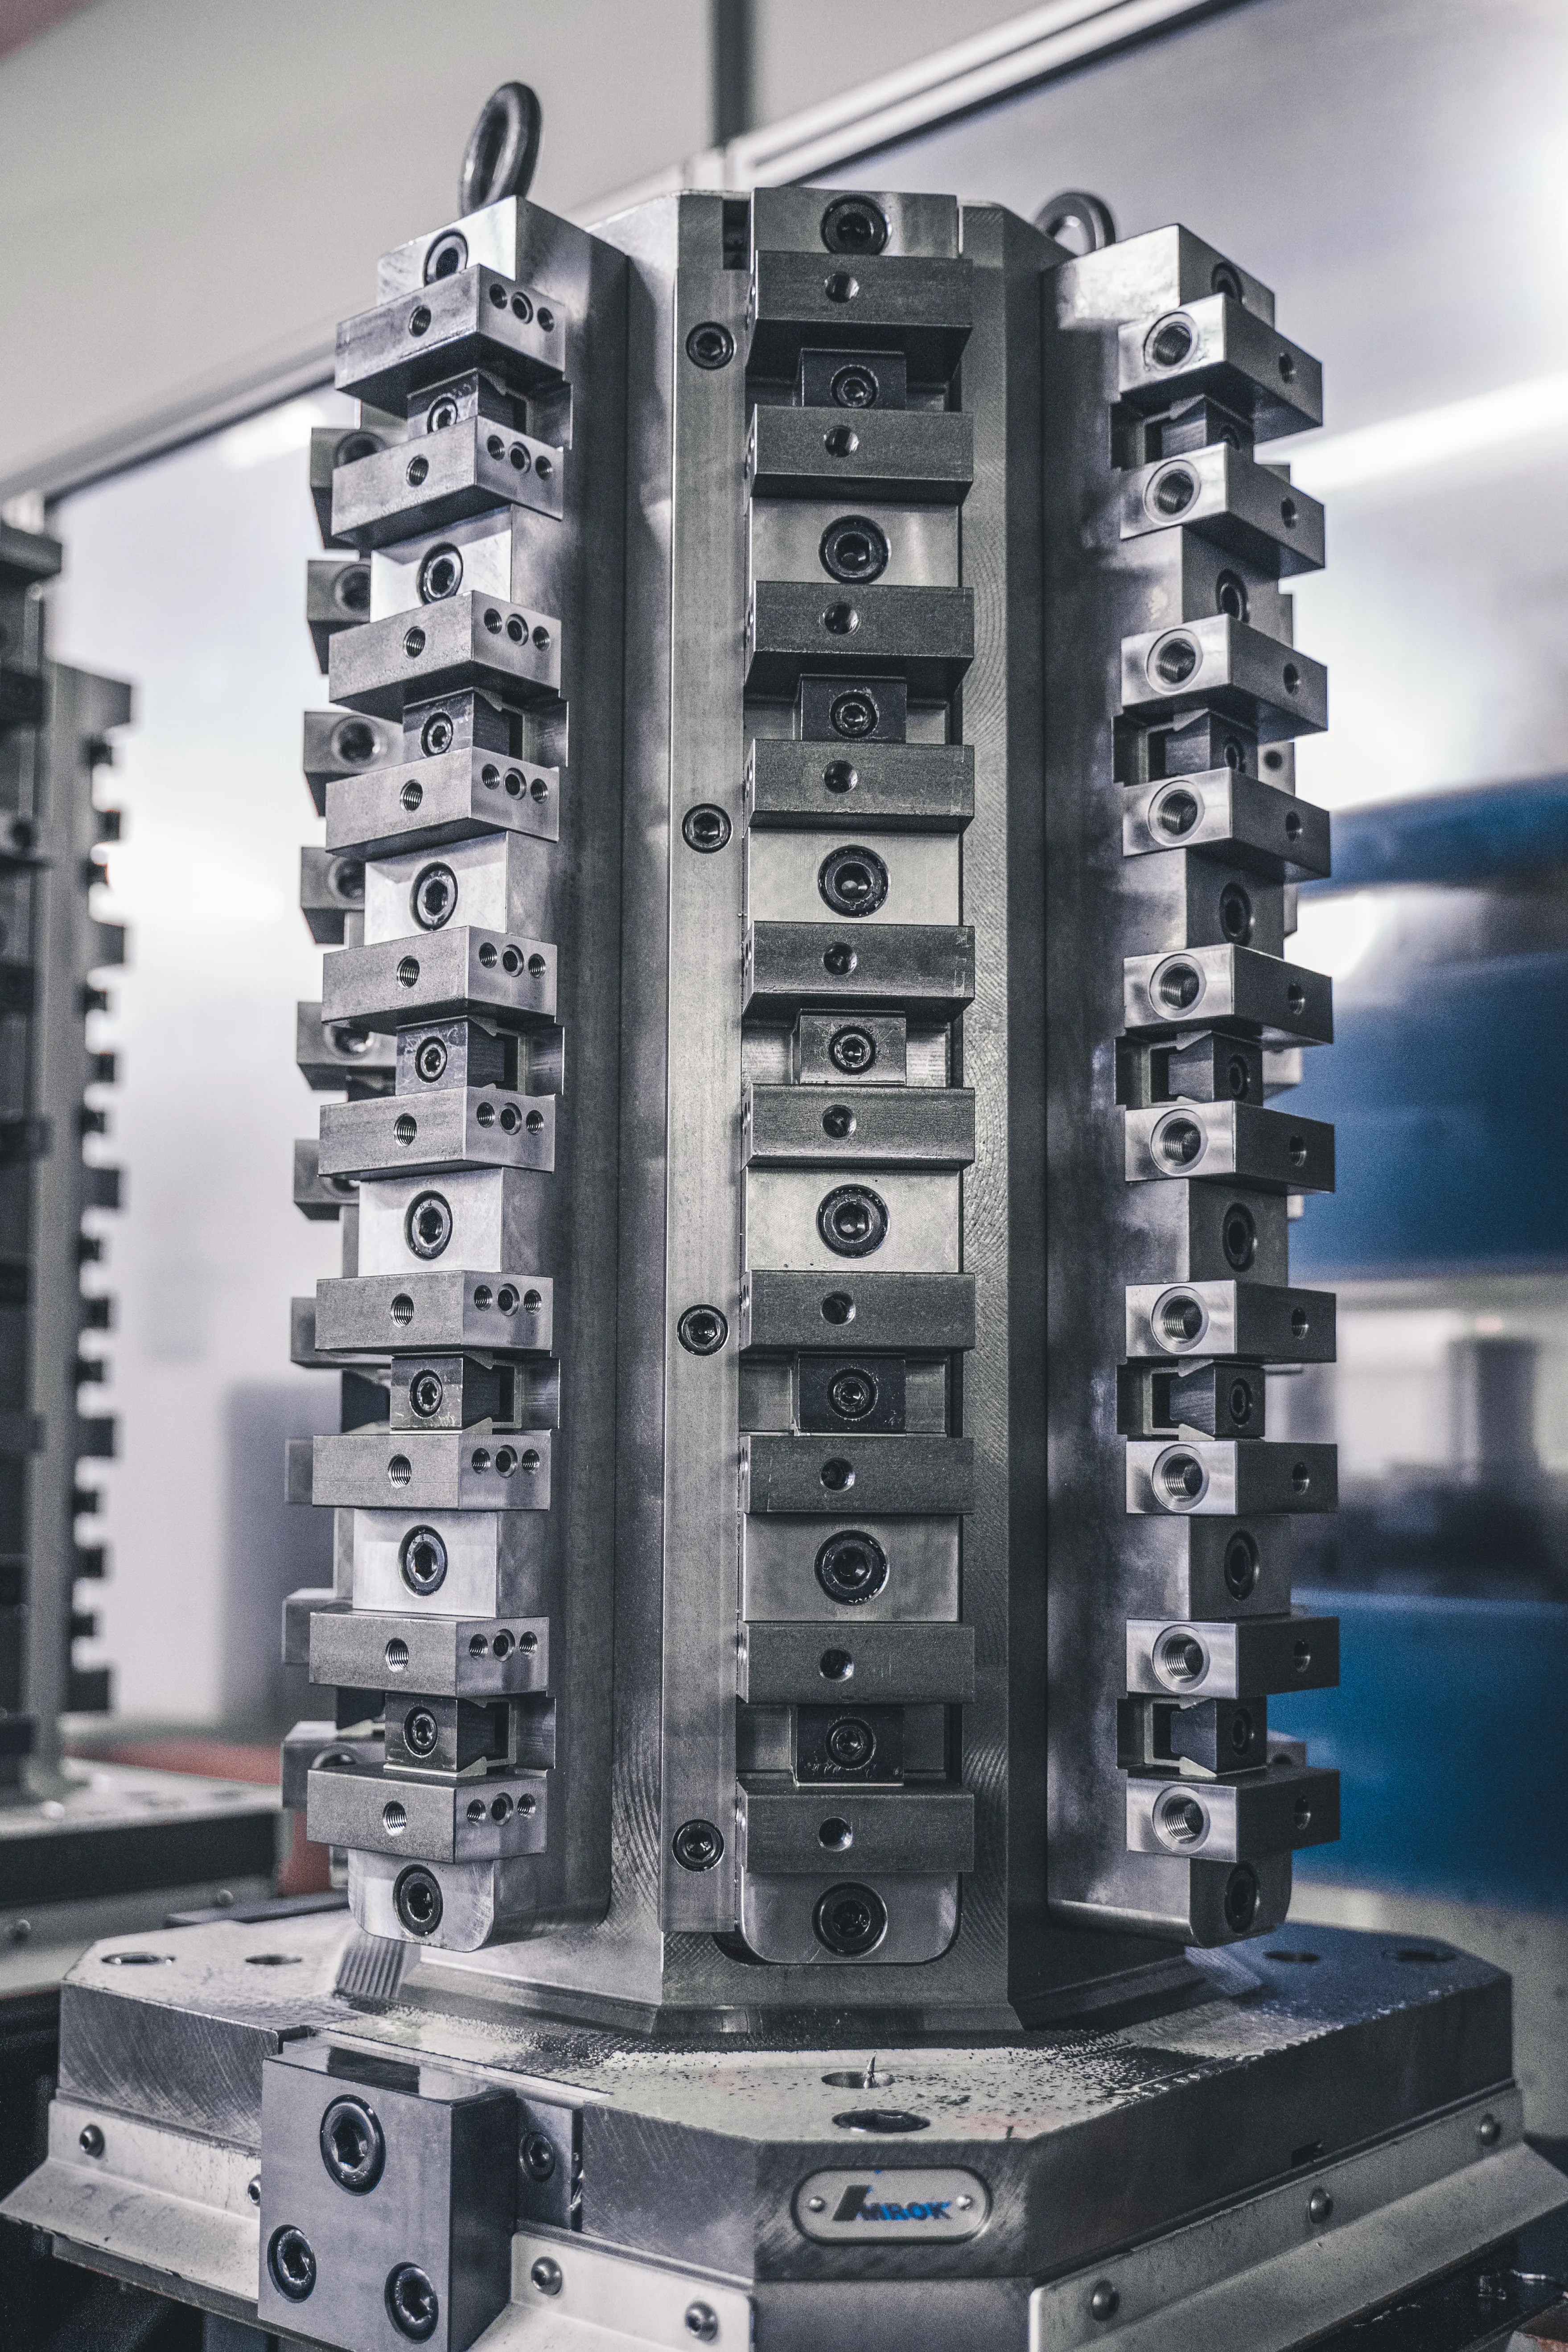
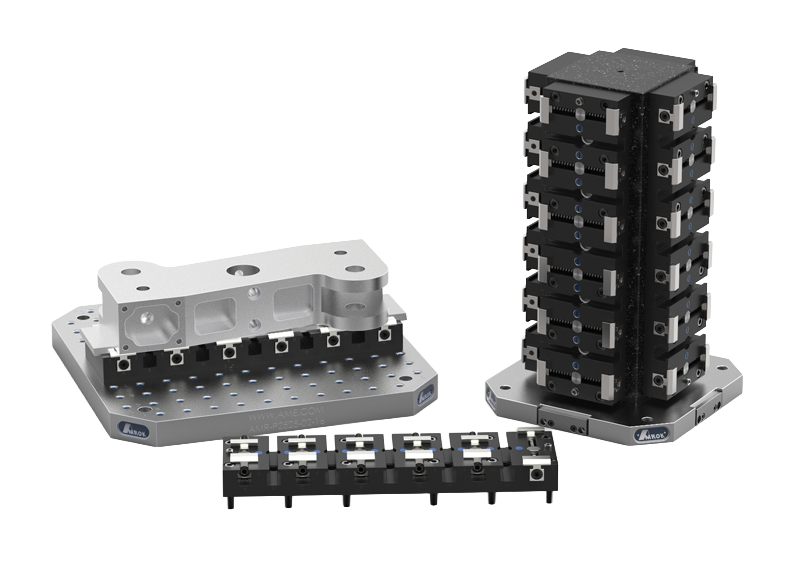
Finding the Right Tombstone is Easy with Hennig
Read our handy guide on how to select the right tombstone from their wide range of products.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.

Hennig Power Protection is a dedicated division specializing in custom-engineered generator enclosures, fuel systems, and power infrastructure for mission-critical applications across data centers, healthcare, telecommunications, and industrial facilities.
Precision machining, fabrication & welding services from our Rockford, IL facility. Complete manufacturing solutions with ISO-certified quality.
Precision machining for turbine...
Pallet delivery, robotic tending & software for lights-out production
CNC machining centers, lathes, grinders & multi-axis equipment
Safety systems & rod locks for hydraulic & mechanical presses
5th Axis double-station vises are optimized for 3-axis machinists to maximize part density per cycle while operating at top efficiency. The flexible design allows shops to convert the double-station vise into a single position fixed jaw by removing the center jaw with just two bolts. Quickly change jaws between hardened steel, machinable steel, and machinable aluminum based on the application.
| Key Features | |
| Part Adaptability | Friction pins allow for independent movement of the jaws on the lead screw while still providing maximum clamping force. |
| Reversible Jaws | Easily reverse the jaws to accommodate larger parts. |
| Single Station Conversion | Easily convert the double-station vise to a single-station for additional clamping range and versatility. |
| Product ID | 3D CAD | Mounting Pattern (mm) | Vise Height (mm) | Vise Width (mm) | Vise Depth (mm) | Jaw Width (mm) | Material | 96 mm Adapted (1x Vise) Part Number | 96 mm Adapted (2x Vises) Part Number | |
|---|---|---|---|---|---|---|---|---|---|---|
| DV56-J1 | 96 | 125.73 | 152.4 | 72.9 | 75 | Hardened Steel | - | - | ||
| DV56-J2 | 96 | 125.73 | 152.4 | 72.9 | 75 | Machinable Aluminum | - | - | ||
| DV56-J3 | 96 | 125.73 | 152.4 | 72.9 | 75 | Machinable Steel | - | - | ||
| DV510-J1 | 96 | 125.73 | 258.3 | 73.4 | 125.7 | Hardened Steel | - | - | ||
| DV510-J2 | 96 | 125.73 | 258.3 | 73.4 | 125.7 | Machinable Aluminum | - | - | ||
| DV510-J3 | 96 | 125.73 | 258.3 | 73.4 | 125.7 | Machinable Steel | - | - | ||
| DV510-J4 | 96 | 125.73 | 258.3 | 73.4 | 125.7 | Hardened Steel* | - | - | ||
| DV75150X-J1 | 52 | 75 | 150 | 56 | 75 | Hardened Steel | R96-DV75150X-J1 | R96-2DV75150X-J1 | ||
| DV75150X-J2 | 52 | 75 | 150 | 56 | 75 | Machinable Aluminum | R96-DV75150X-J2 | R96-2DV75150X-J2 | ||
| DV75150X-J3 | 52 | 75 | 150 | 56 | 75 | Machinable Steel | R96-DV75150X-J3 | R96-2DV75150X-J3 |
Each model below is routed to the best next step based on availability.
Every changeover means idle spindle time. Multi-part fixturing slashes setup frequency — so your machines spend more hours cutting and less time waiting.
Based on 250 working days/yr. Multi-part fixturing reduces changeover frequency so your spindle spends more time cutting.
Read our handy guide on how to select the right tombstone from their wide range of products.
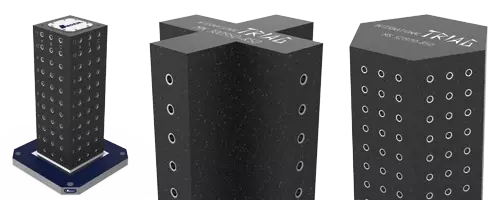
Dr. Tony Schmitz, a professor specializing in vibration analysis, came to AME to do a series of tests on the various material types of tombstones and breaks down his findings to determine the best type of tombstone for your shop.
If you want to reduce your overall costs and increase your flexibility to meet your customers’ demands, consider incorporating off-machine set-ups into your machining process.
Both Hennig and its sister company, Advanced Machine & Engineering, now operate under the Hennig brand.
Same team. Same products. Same company. Different look.
Unifying the two brands under one name clarifies our offerings and makes them easier for you to navigate — one website, one team, one trusted partner.