Machine Tool Ecosystem

Magnetic Conveyors

Intended for ferrous material applications with chips (40 micron and above), small parts, or scraps.

Magnetic Chip Conveyors

Conveyors for ferrous material

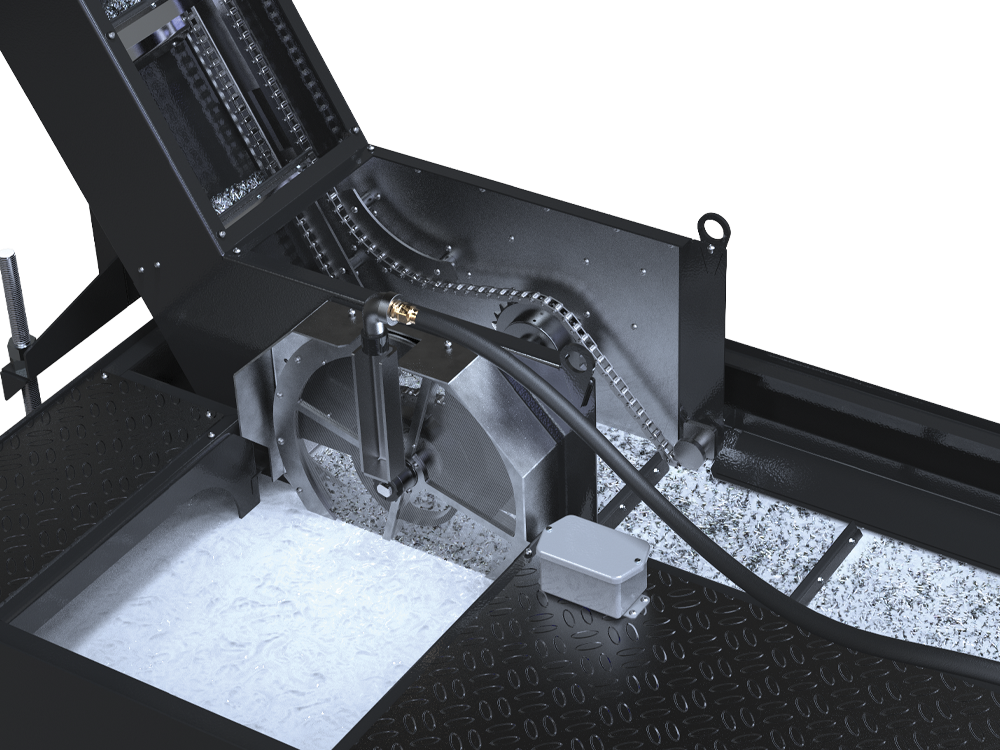
Intended for ferrous material applications with chips (40 micron and above), small parts, or scraps. Our closed oil system lubricates all internal parts automatically, resulting in minimal maintenance, no oil refills, no manually lubricating bearings or bushings. All magnetic conveyors can be custom designed to suit your application, with widths from 102 mm to 1066 mm available and systems that can handle a range of 0 lbs to 12,000 lbs per hour.

Common Applications
Environment Wet or dry applications
Chip types Fines, small or broken chips, swarf (particles 40 microns or larger)
Parts & large stampings Up to 8" (203 mm) long. Larger parts require samples and testing. Typically limited by conveyor width.
Central conveyor system When all material is ferrous
Features
Closed oil system Never needs to be filled or maintained
Heavy-duyty die springs Keeps infeed sprocket and tail shaft adjusted properly
Sunflower based oil  
High temperature resistance Rare earth magnets up to 176°F.  Ceramic magnets up to 450°F. Magnet strength declines above these temps.
Conveyor speed (ft/min) 25, 30, 45, 60
Standard incline angles 30°, 45°, 60°, 75°, 90°
Motor voltage 110, 230, 460, 575
Options
Coolant tank  
Coolant filtration  
Part de-magnetizer  
Dimpled slider bed To prevent hydro-locking
Manganese slider bed For heavy-duty applications
Custom dishcharge chutes Manual adjust, tipple, various angles
Covered chip chutes  
Casters  

Which Conveyor
Is Right for Me?

Material
Chip Type
Space Constraints
Best Fit

View Details
Machine Uptime Calculator

How Much Are Chip Stops Costing You?

Every time an operator stops a machine to clear chips, you lose production revenue. Quantify the problem — then see how a conveyor pays for itself.

Your Setup
$
The Chip Problem
min
Annual Impact of Manual Chip Clearing
750 hrs
Production Hours Lost / Year
$131K
Annual Lost Revenue
$112K
Recoverable with Conveyor
See Full ROI Breakdown

Based on 250 working days/yr and 85% recovery — conveyors eliminate most manual chip clearing stops.

From the Resource Hub

Related Articles

The Rundown on Hennig’s Integrated Through-Spindle Coolant System
Blogs Chip & Coolant Management Product Selection

The Rundown on Hennig’s Integrated Through-Spindle Coolant System

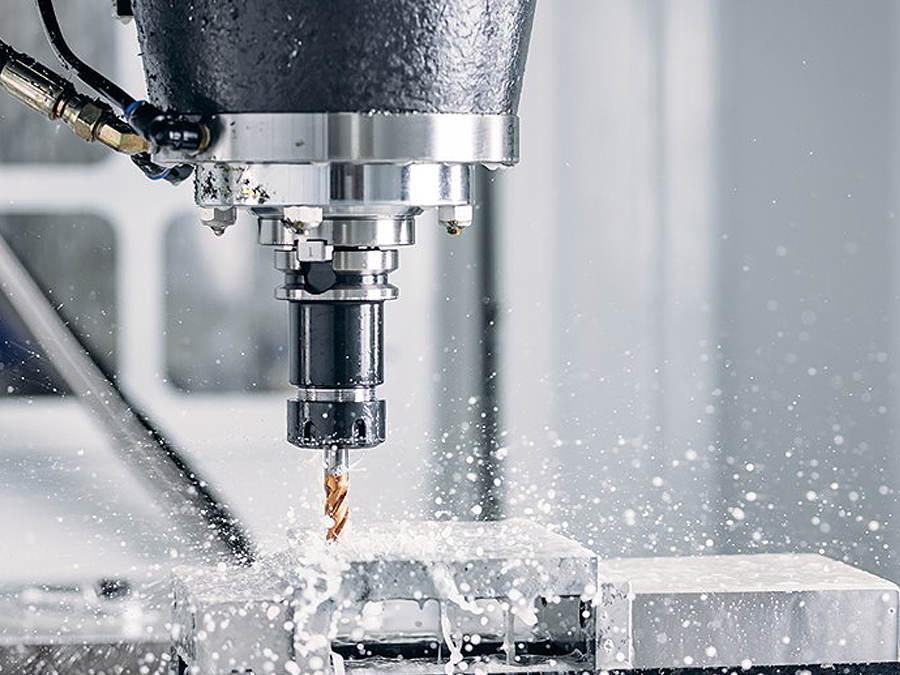
Through-spindle coolant systems hit the bullseye when it comes to reducing the friction between the tool and the workpiece during machining. But contaminants in the coolant can work against you, wearing down tools and ruining the surface finish of the part. That’s why Hennig developed an integrated high-pressure coolant systems for through-spindle coolant applications.
Chip Disc Filtration: The Unsung Hero of Lights Out Manufacturing Success
Blogs Chip & Coolant Management Product Selection

Chip Disc Filtration: The Unsung Hero of Lights Out Manufacturing Success

If lights out manufacturing is your goal, Hennig's chip filtration expertise will help you achieve it with our patented Chip Disc Filtration (CDF) system.

Why You Should Select a VFD Control for Your Hennig Conveyor
Blogs Chip & Coolant Management Product Selection

Why You Should Select a VFD Control for Your Hennig Conveyor

Due to the ever-increasing demand for improved chip conveyor functionality and efficiency, Hennig has offered VFD's (Variable Frequency Drives) as a standard for most new conveyor products for several years. Learn some of the many advantages to this approach in conveyor design.