



Blogs
Workholding
Product Selection
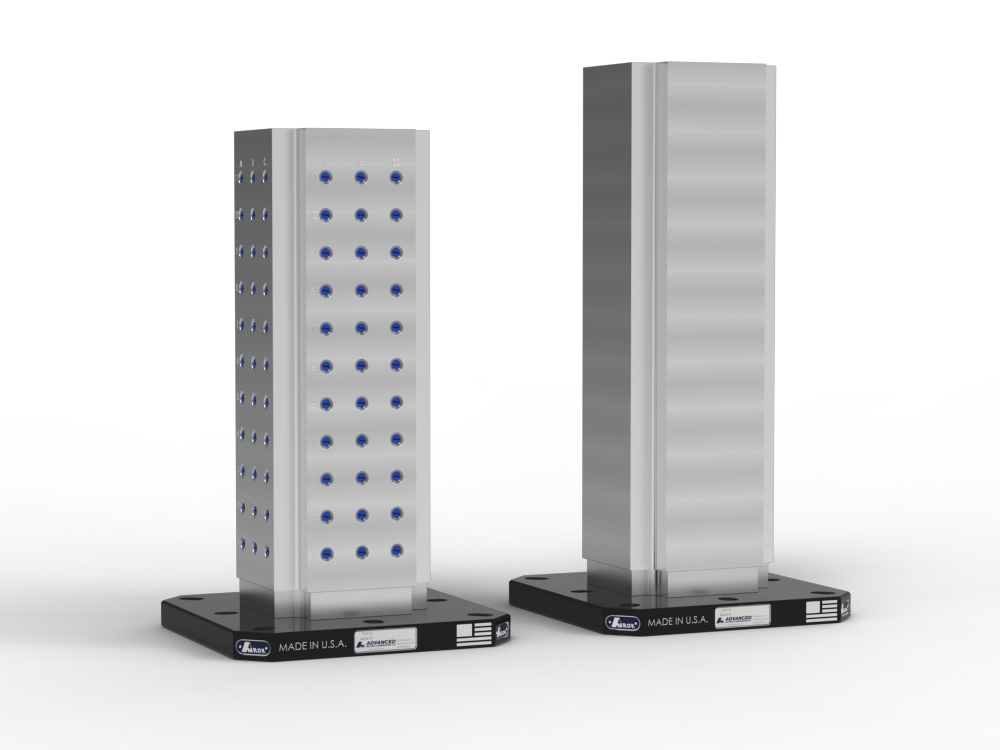
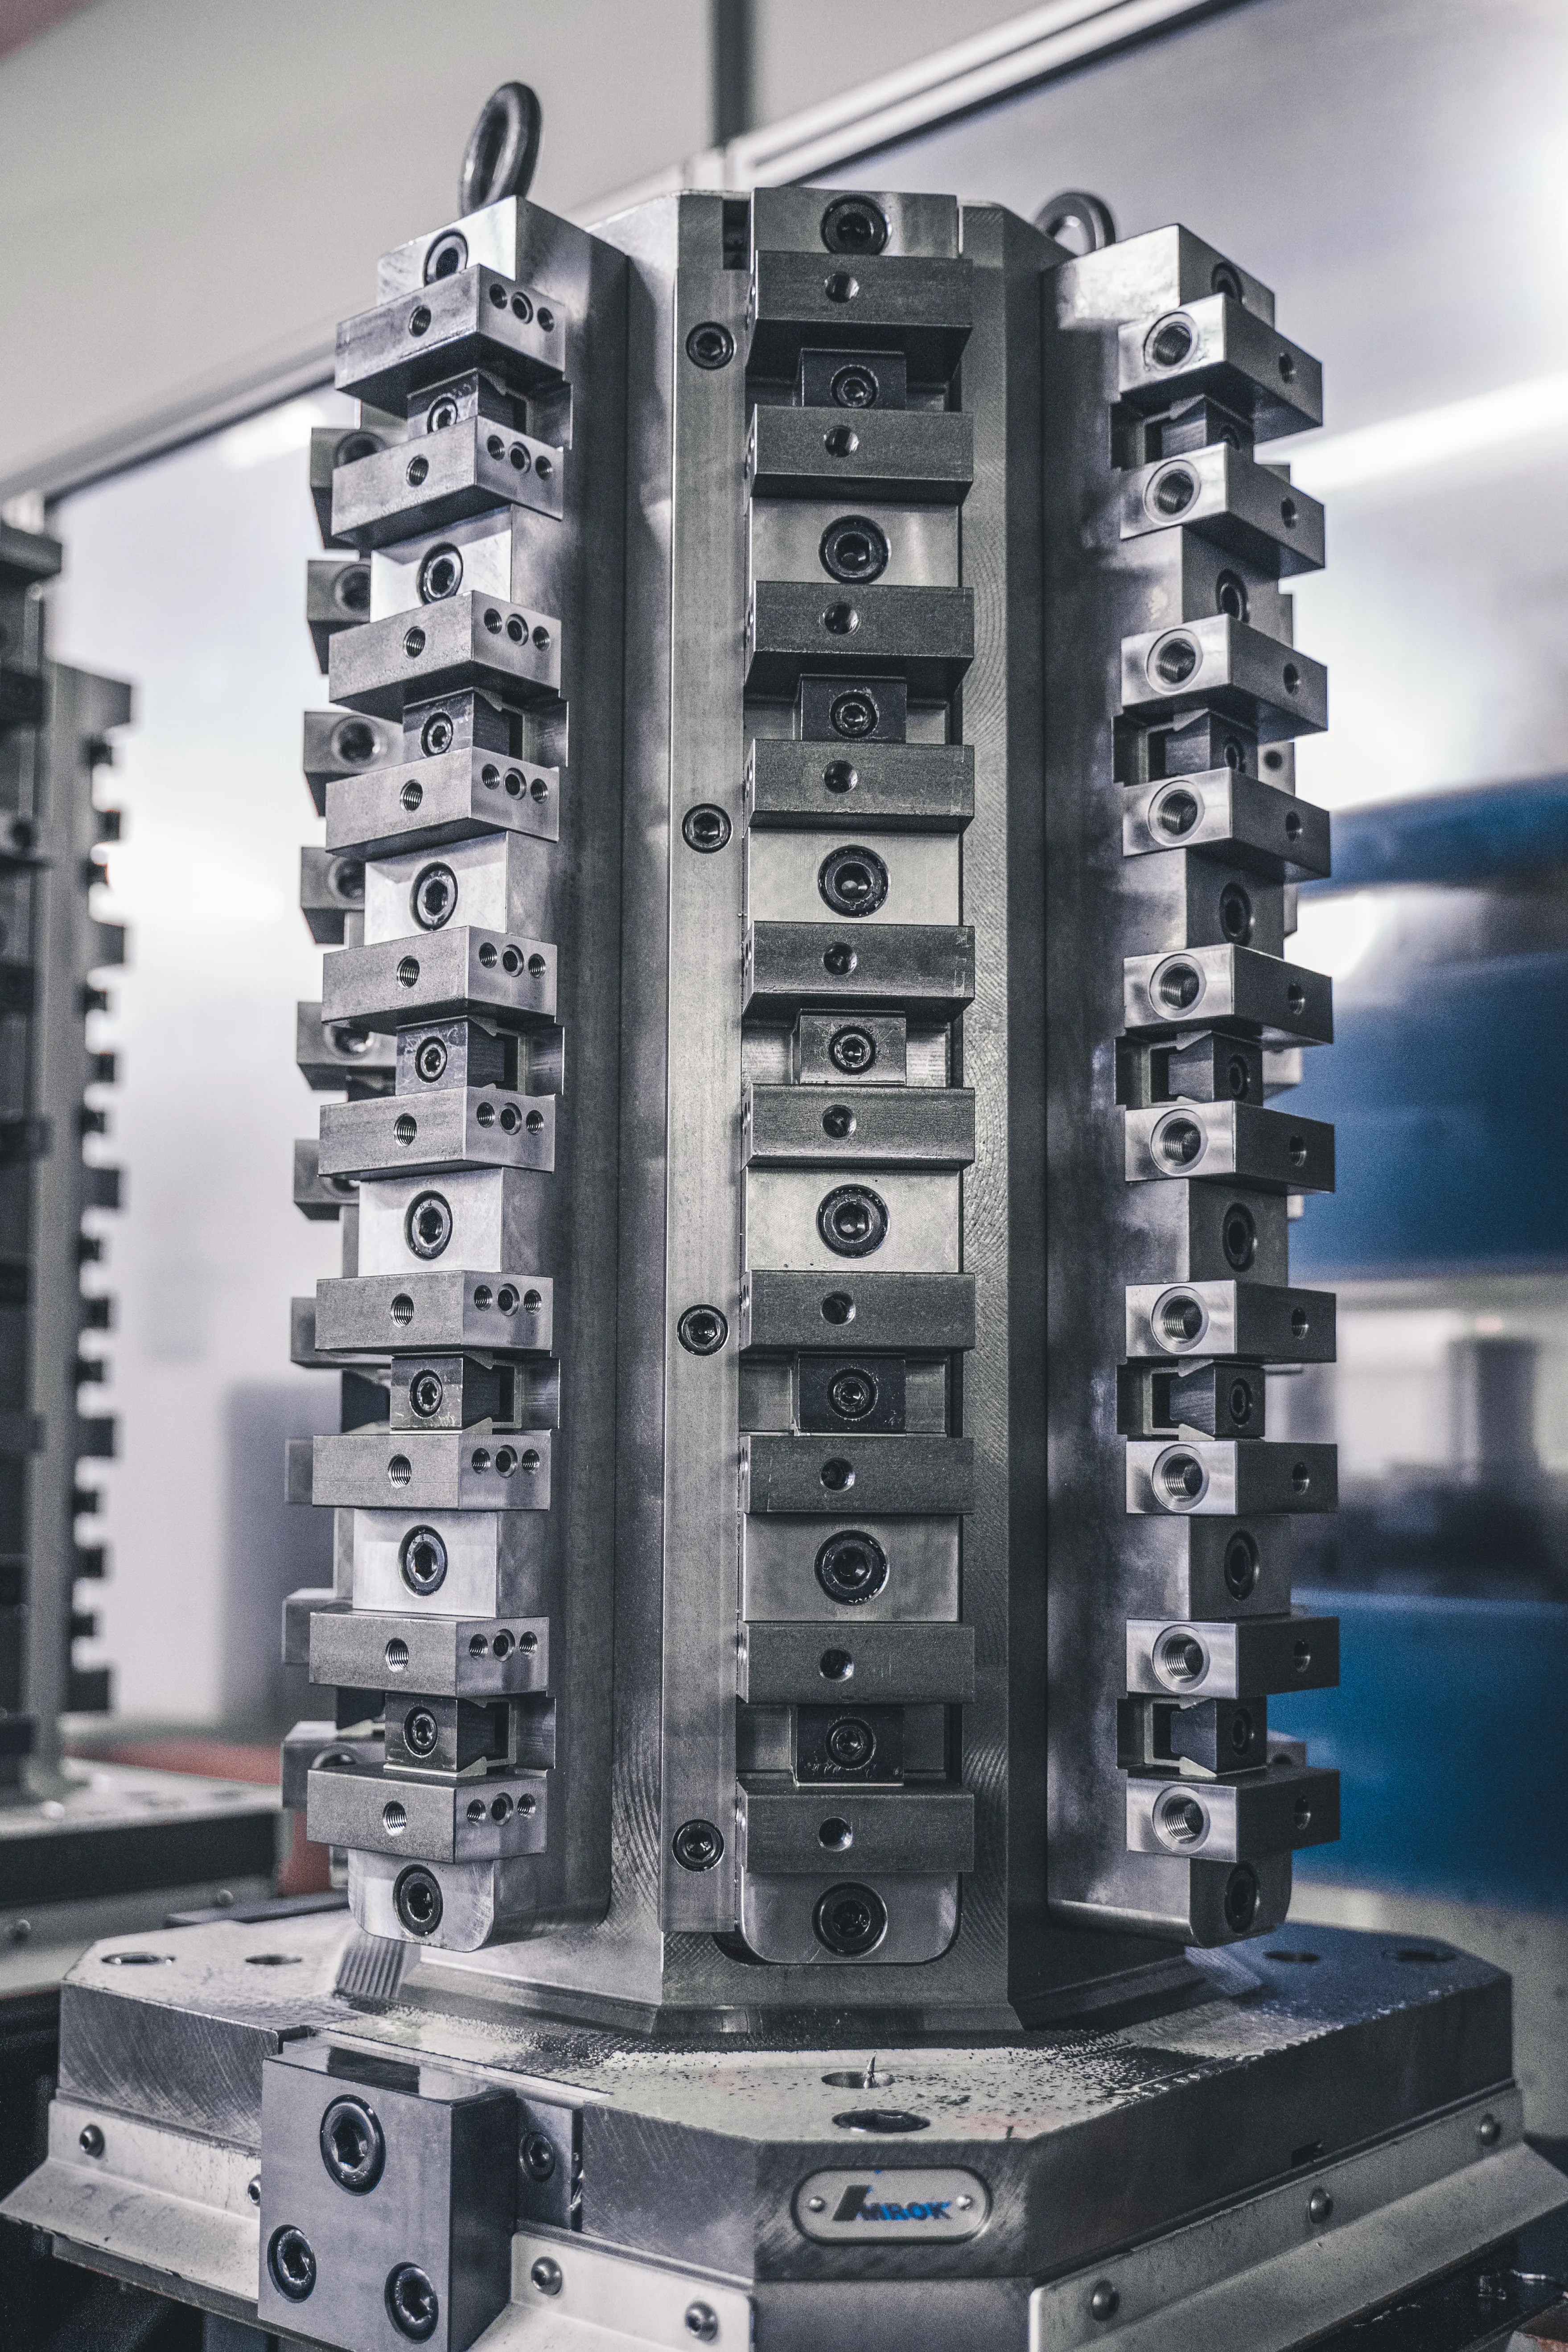
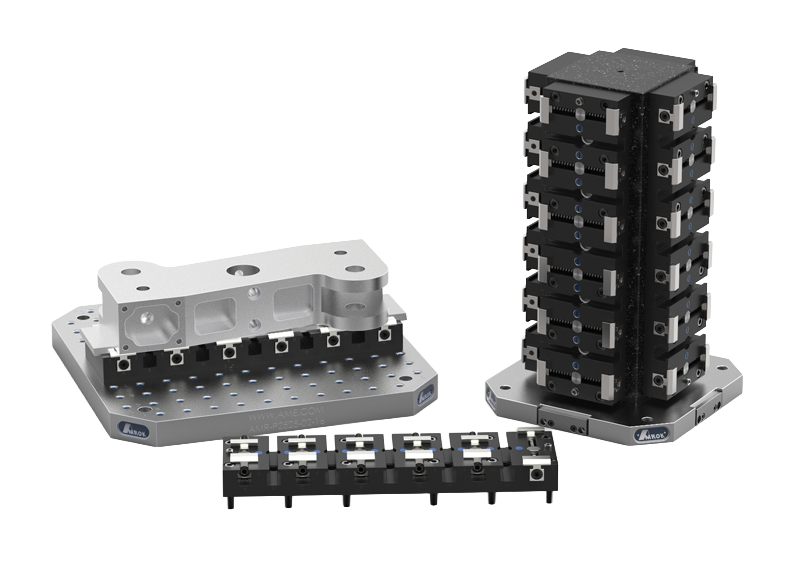
Finding the Right Tombstone is Easy with Hennig
Read our handy guide on how to select the right tombstone from their wide range of products.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.

Hennig Power Protection is a dedicated division specializing in custom-engineered generator enclosures, fuel systems, and power infrastructure for mission-critical applications across data centers, healthcare, telecommunications, and industrial facilities.
Precision machining, fabrication & welding services from our Rockford, IL facility. Complete manufacturing solutions with ISO-certified quality.
Precision machining for turbine...
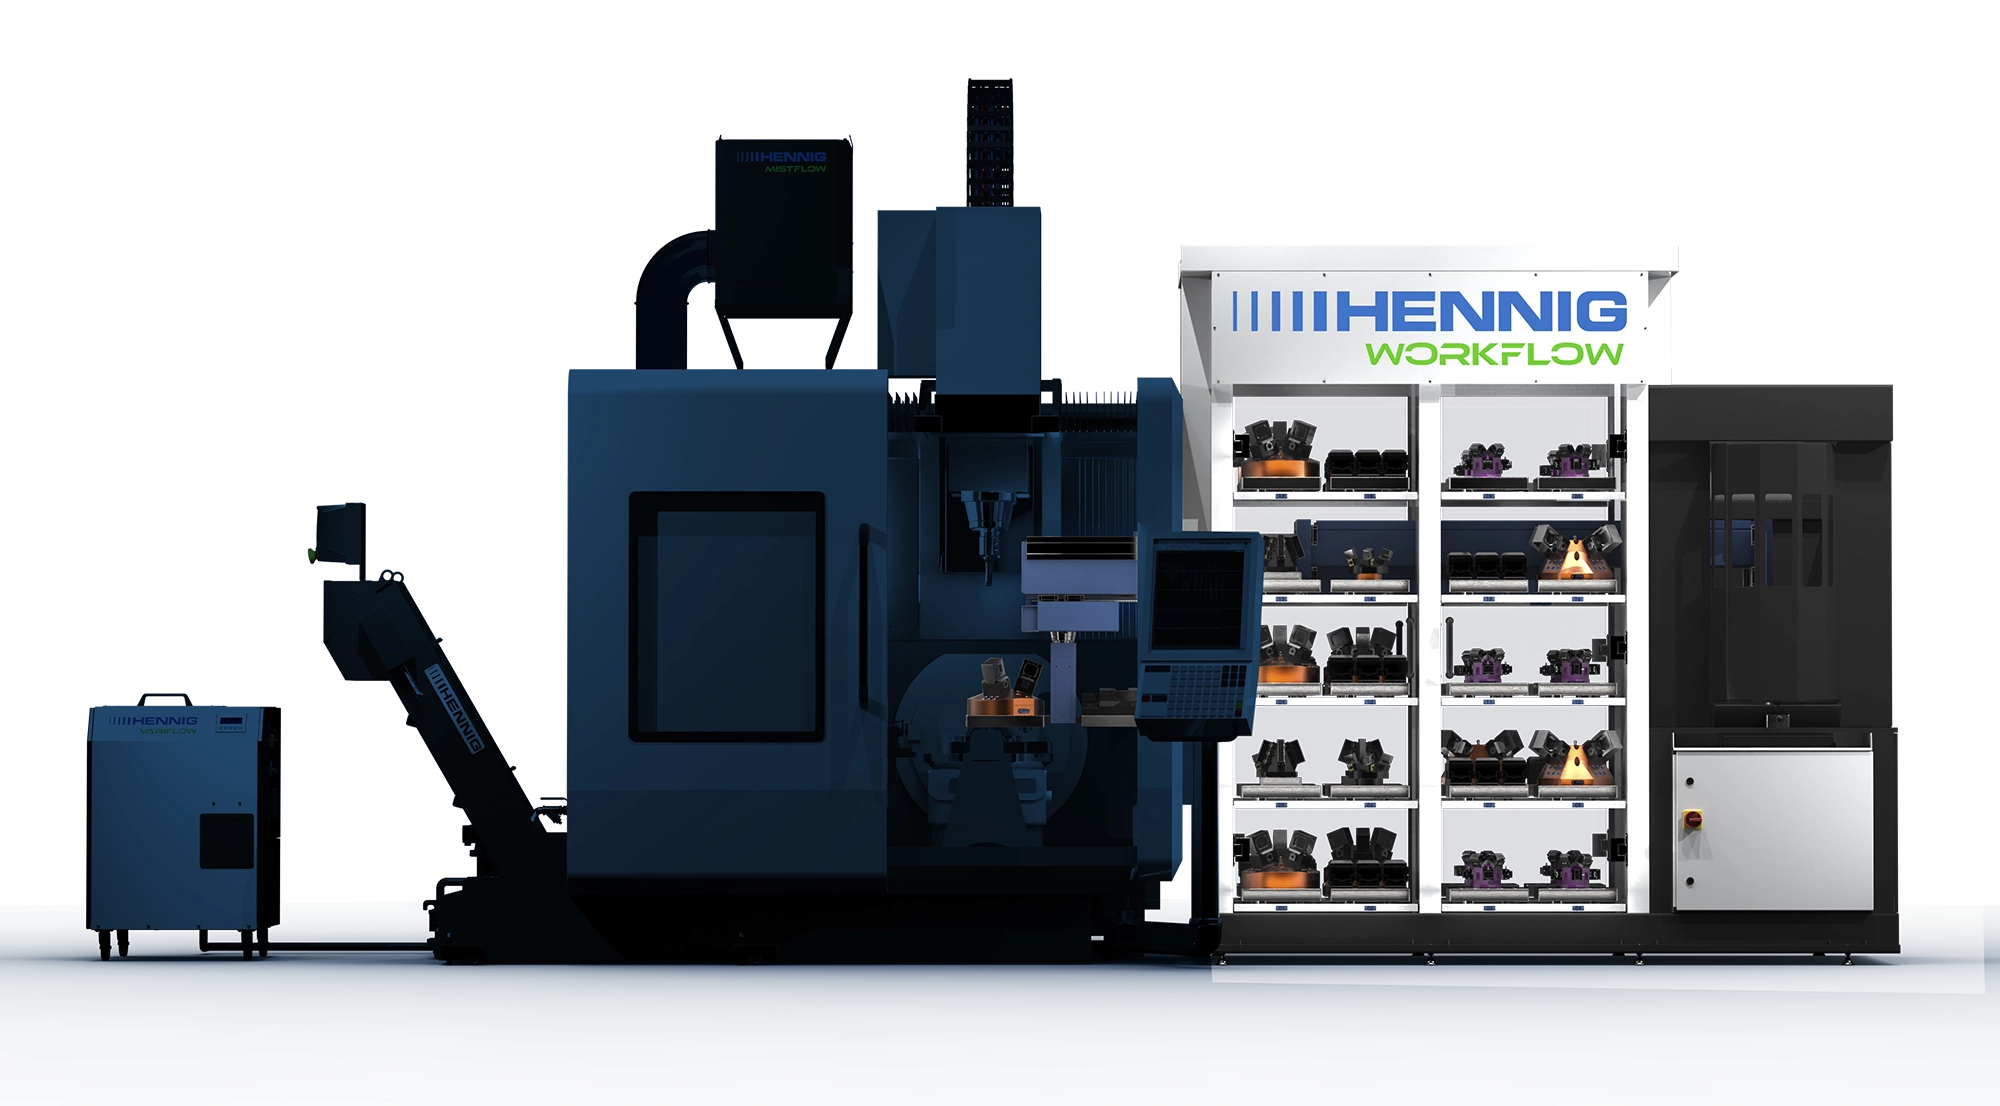
Pallet delivery, robotic tending & software for lights-out production
CNC machining centers, lathes, grinders & multi-axis equipment
Safety systems & rod locks for hydraulic & mechanical presses
Table dimensions aren't available for this model.
Select a pallet size directly, or contact us for help matching your machine.
Grid plates are developed as a low-profile CNC subplate equipped with a precision, alphanumeric 2” grid pattern. Installed directly to your CNC machine table, these grid plates are made to meet the tightest industry tolerances and are equipped for use with any 2” compatible workholding system.
| Key Features |
| Grid holes, bushings, and inserts are available for both 1/2" and 5/8" systems |
| Hardened, threaded inserts allow for clamping in every hole while offering quick and easy replaceability |
| Hardened, precision bushings are accurately located to ensure easy locating coupled with high wear resistance |
| Replacement bushings and insert kits with an extraction tool are available upon request |
Grid plates are also known as: Tooling Plates, Sub Plates, or Locator Plates
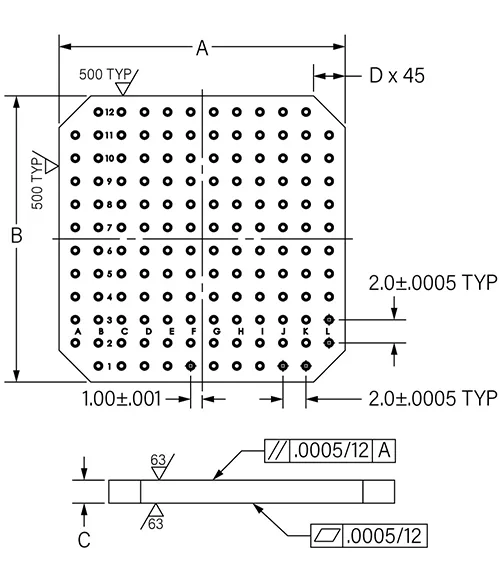
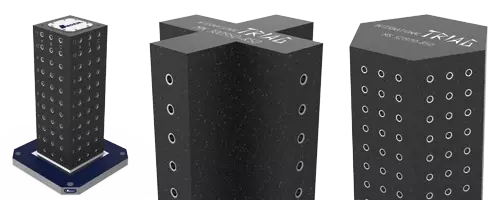
CAD Downloads: CAD download is for a plain face tombstone, all measurements are in inches unless otherwise noted, all weights are in pounds and include base plate.
| Tolerance | Precision |
| Flatness (tombstones & plates) | 0.0005 / 12x12 |
| Parallelism (plates) | .0005 / 12 Max .002 total |
| Perpendicularity | .0008 / 12 Min .001, Max .002/48 |
| Surface Finish | 63 RMS |
| Face Thickness | ≤18” = ±.002, >18” = ±.003 |
| Tapped Holes (non-accumulative) | ±.005 |
| Precision Bushing I.D. | +0.0013 / +0.0007 |
| Precision Bushing Concentricity | 0.0001 |
| Bored or Precision Bushing Hole to Adjacent Hole | ±0.0005 |
| First Row Bushing Hole Location from Datums | ±.002 |
| Bored or Precision Bushing Hole Spacing (non-accumulative) | 0-10 ±.0005*, 10-20 ±.0008, 20-30 ±.0010, 30-40 ±.0012 |
*For aluminum, add 50% to these tolerances.
| Product ID | 3D CAD | Buy Online | A (in) | B (in) | C (in) | D (in) | Weight-Aluminum (lbs) | Weight-Steel (lbs) | Number of Holes | Grid Style | |
|---|---|---|---|---|---|---|---|---|---|---|---|
| AMR-P1616-02-50 | 15.75 (400mm) | 15.70 (400mm) | 1.97 (50mm) | 11.811 (300mm) to 12.598 (320mm) | 38 | 105 | 60 | UNC 1/2"-13 | |||
| AMR-P2016-02-50 | 19.69 (500mm) | 15.70 (400mm) | N/A | Upon Request | 60 | 165 | 76 | UNC 1/2"-13 | |||
| AMR-P2016-02-62 | 19.69 (500mm) | 15.70 (400mm) | N/A | Upon Request | 60 | 165 | 76 | UNC 5/8"-11 | |||
| AMR-P2020-02-50 | 19.69 (500mm) | 19.60 (500mm) | 2.36 (60mm) | 15.748 (400mm) to 16.000 (406.4mm) | 75 | 206 | 96 | UNC 1/2"-13 | |||
| AMR-P2020-02-62 | 19.69 (500mm) | 19.60 (500mm) | 2.36 (60mm) | 15.748 (400mm) to 16.000 (406.4mm) | 75 | 206 | 96 | UNC 5/8"-11 | |||
| AMR-P2520-02-50 | 24.80 (630mm) | 19.60 (500mm) | N/A | Upon Request | 95 | 262 | 116 | UNC 1/2"-13 | |||
| AMR-P2520-02-62 | 24.80 (630mm) | 19.60 (500mm) | N/A | Upon Request | 95 | 262 | 116 | UNC 5/8"-11 | |||
| AMR-P2525-02-50 | 24.80 (630mm) | 24.80 (630mm) | 2.76 (70mm) | 19.685 (500mm) to 20.000 (508mm) | 120 | 331 | 140 | UNC 1/2"-13 | |||
| AMR-P2525-02-62 | 24.80 (630mm) | 24.80 (630mm) | 2.76 (70mm) | 19.685 (500mm) to 20.000 (508mm) | 120 | 331 | 140 | UNC 5/8"-11 | |||
| AMR-P3225-02-50 | 31.50 (800mm) | 24.80 (630mm) | N/A | Upon Request | 181 | 498 | 188 | UNC 1/2"-13 | |||
| AMR-P3225-02-62 | 31.50 (800mm) | 24.80 (630mm) | N/A | Upon Request | 181 | 498 | 188 | UNC 5/8"-11 | |||
| AMR-P3232-02-50 | 31.50 (800mm) | 31.50 (800mm) | 3.94 (100mm) | 25.000 (635mm) to 25.197 (640mm) | 227 | 625 | 244 | UNC 1/2"-13 | |||
| AMR-P3232-02-62 | 31.50 (800mm) | 31.50 (800mm) | 3.94 (100mm) | 25.000 (635mm) to 25.197 (640mm) | 227 | 625 | 244 | UNC 5/8"-11 | |||
| AMR-P3920-02-50 | 39.37 (1000mm) | 19.60 (500mm) | N/A | Upon Request | 175 | 481 | 188 | UNC 1/2"-13 | |||
| AMR-P3920-02-62 | 39.37 (1000mm) | 19.60 (500mm) | N/A | Upon Request | 175 | 481 | 188 | UNC 5/8"-11 | |||
| AMR-P3930-02-50 | 39.37 (1000mm) | 29.50 (750mm) | N/A | Upon Request | 218 | 600 | 268 | UNC 1/2"-13 | |||
| AMR-P3930-02-62 | 39.37 (1000mm) | 29.50 (750mm) | N/A | Upon Request | 218 | 600 | 268 | UNC 5/8"-11 |
Each model below is routed to the best next step based on availability.
Every changeover means idle spindle time. Multi-part fixturing slashes setup frequency — so your machines spend more hours cutting and less time waiting.
Based on 250 working days/yr. Multi-part fixturing reduces changeover frequency so your spindle spends more time cutting.
Read our handy guide on how to select the right tombstone from their wide range of products.
Dr. Tony Schmitz, a professor specializing in vibration analysis, came to AME to do a series of tests on the various material types of tombstones and breaks down his findings to determine the best type of tombstone for your shop.
If you want to reduce your overall costs and increase your flexibility to meet your customers’ demands, consider incorporating off-machine set-ups into your machining process.
Both Hennig and its sister company, Advanced Machine & Engineering, now operate under the Hennig brand.
Same team. Same products. Same company. Different look.
Unifying the two brands under one name clarifies our offerings and makes them easier for you to navigate — one website, one team, one trusted partner.