



Blogs
Workholding
Product Selection
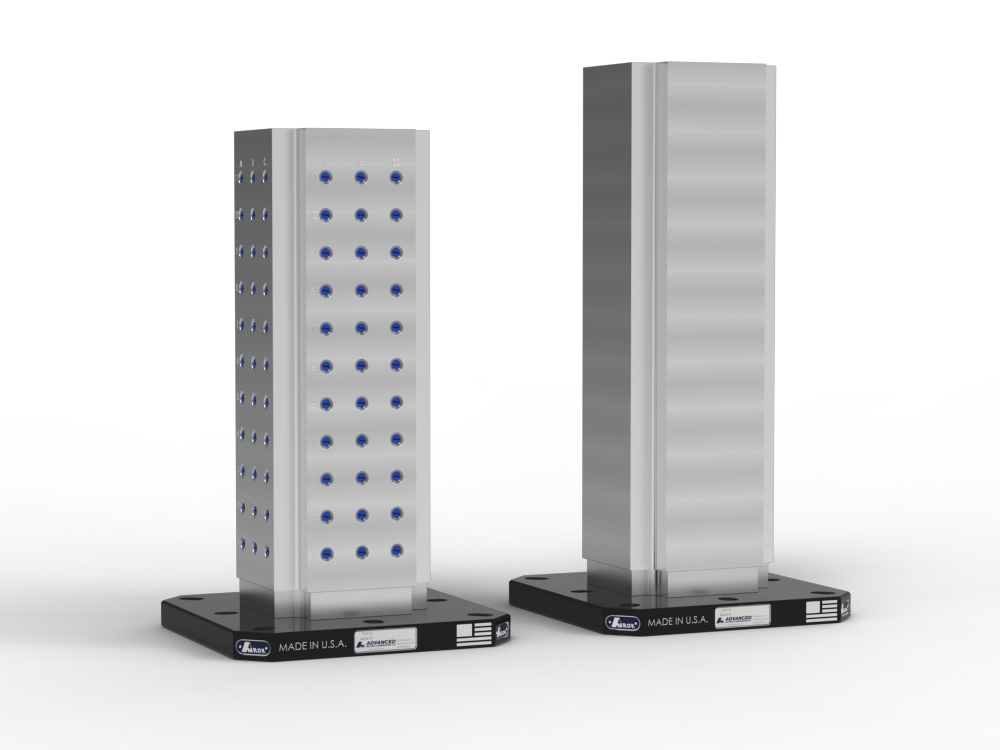
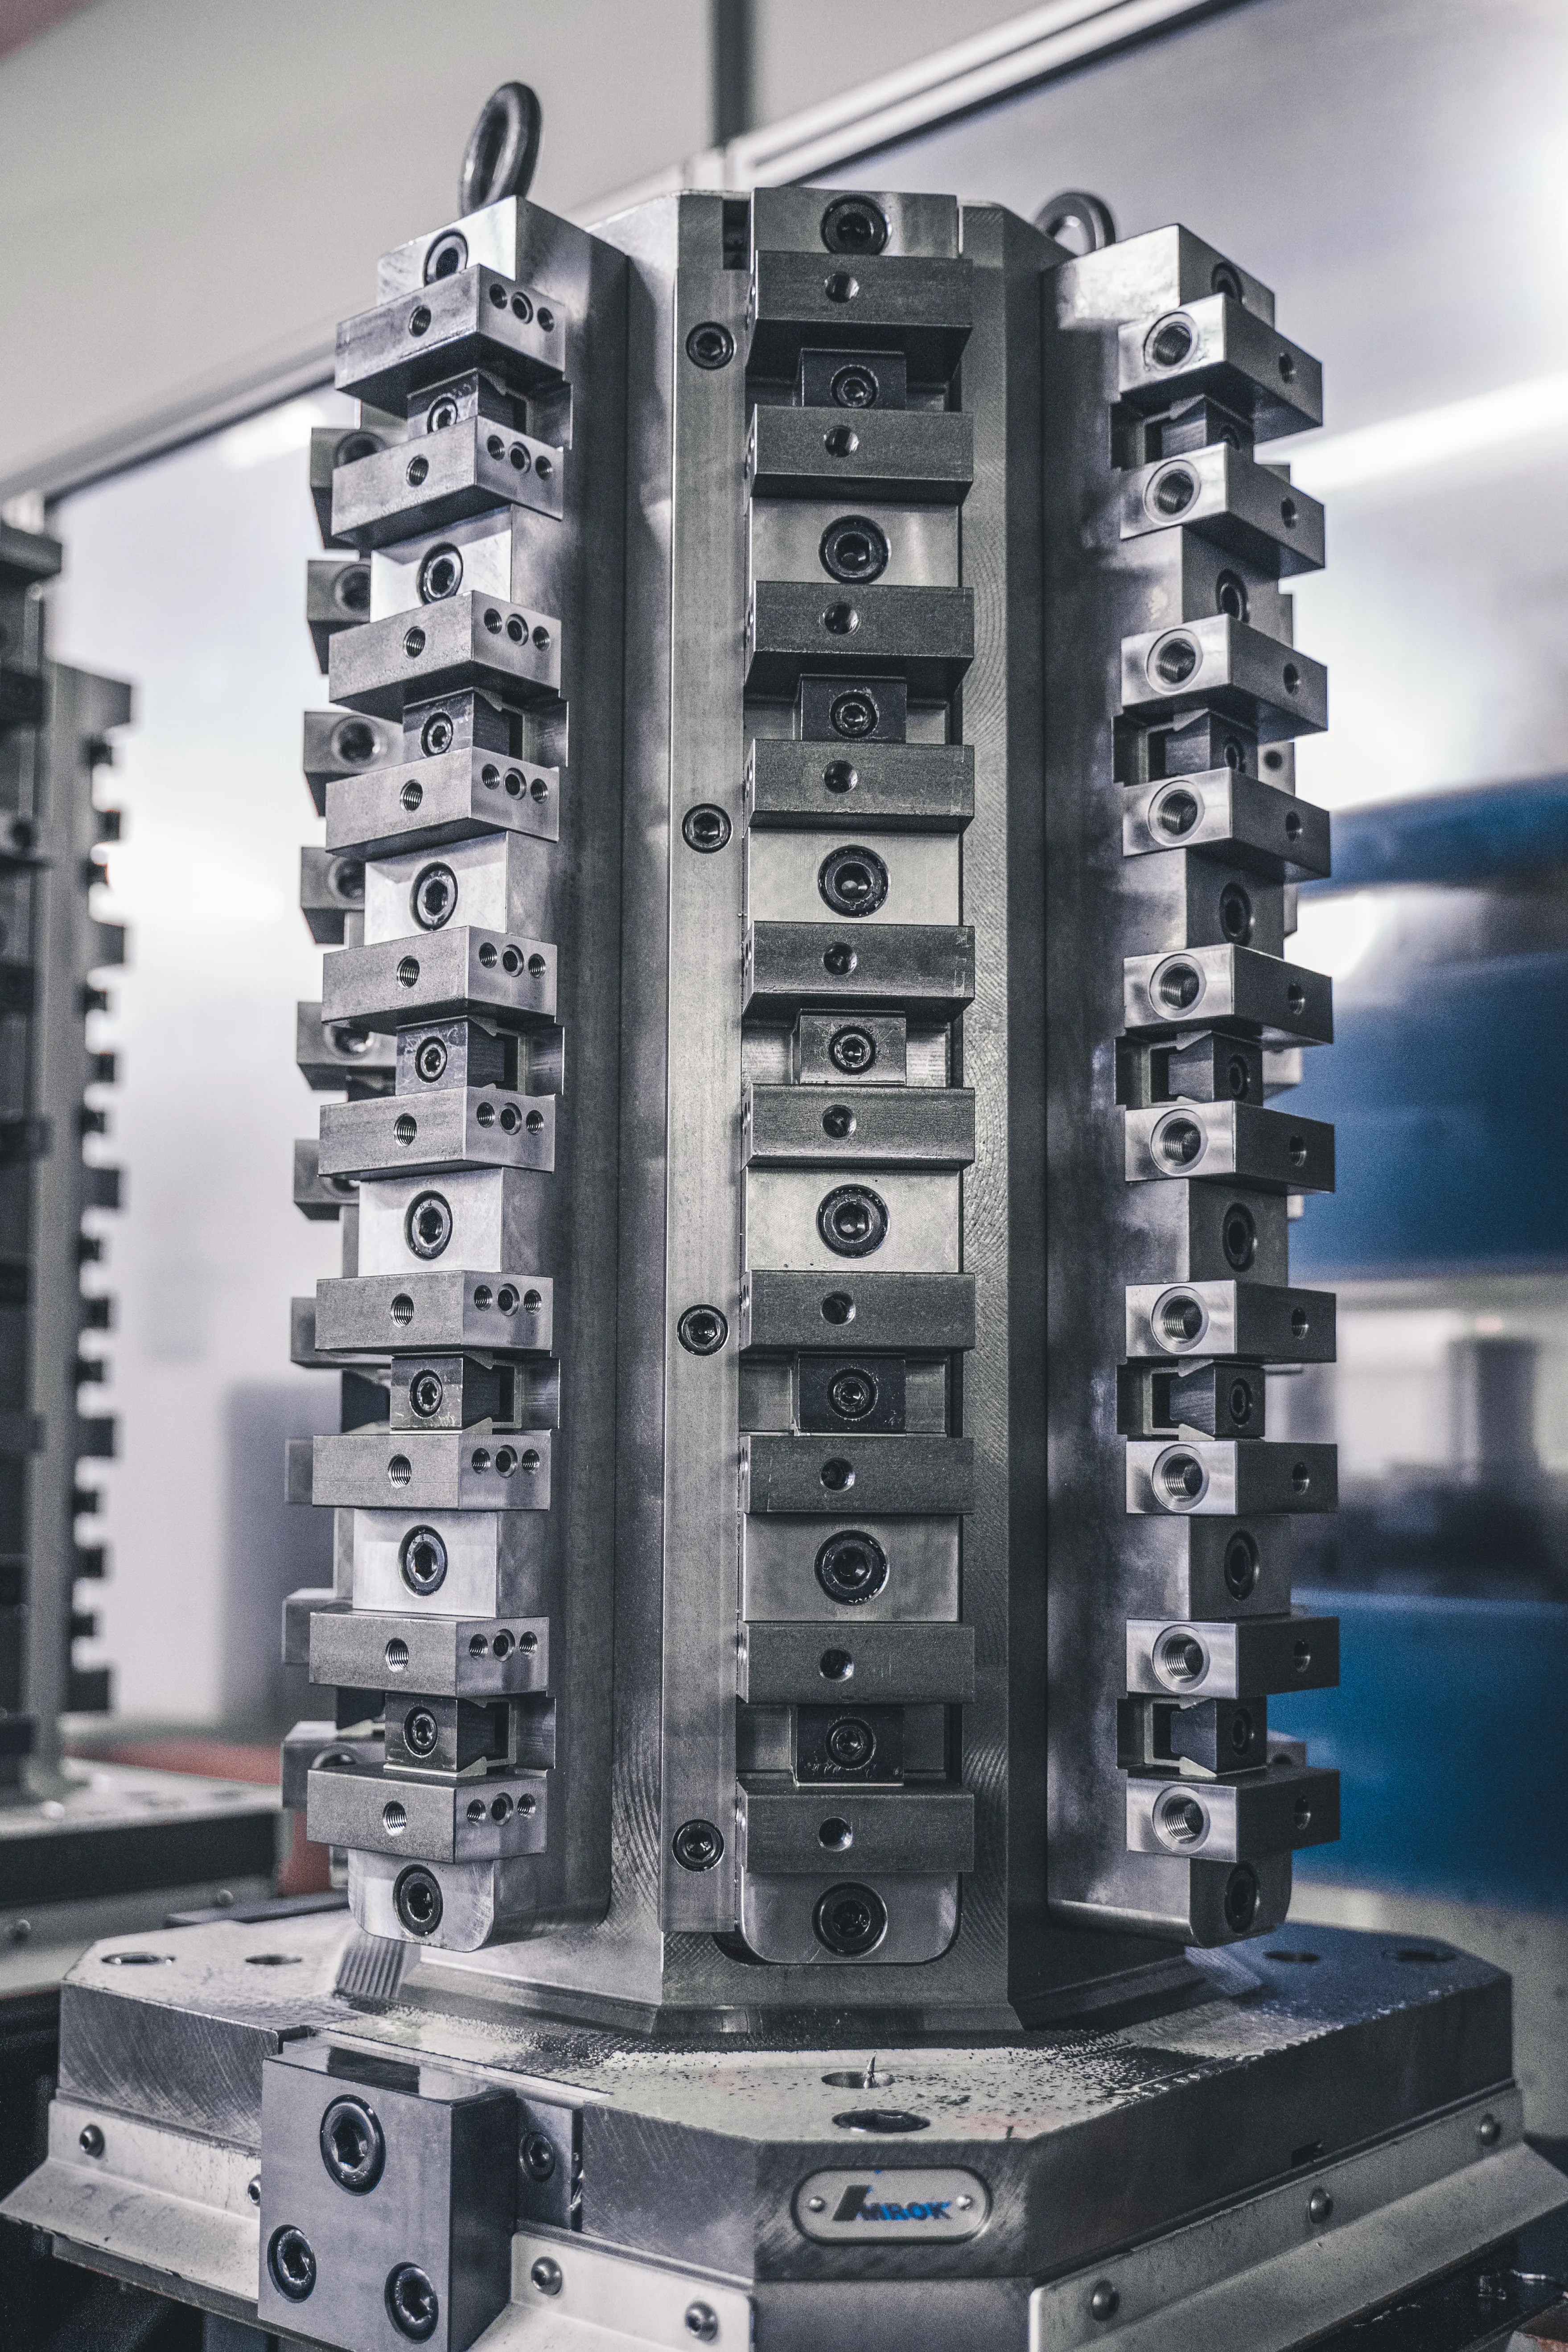
Finding the Right Tombstone is Easy with Hennig
Read our handy guide on how to select the right tombstone from their wide range of products.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.

Hennig Power Protection is a dedicated division specializing in custom-engineered generator enclosures, fuel systems, and power infrastructure for mission-critical applications across data centers, healthcare, telecommunications, and industrial facilities.
Precision machining, fabrication & welding services from our Rockford, IL facility. Complete manufacturing solutions with ISO-certified quality.
Precision machining for turbine...
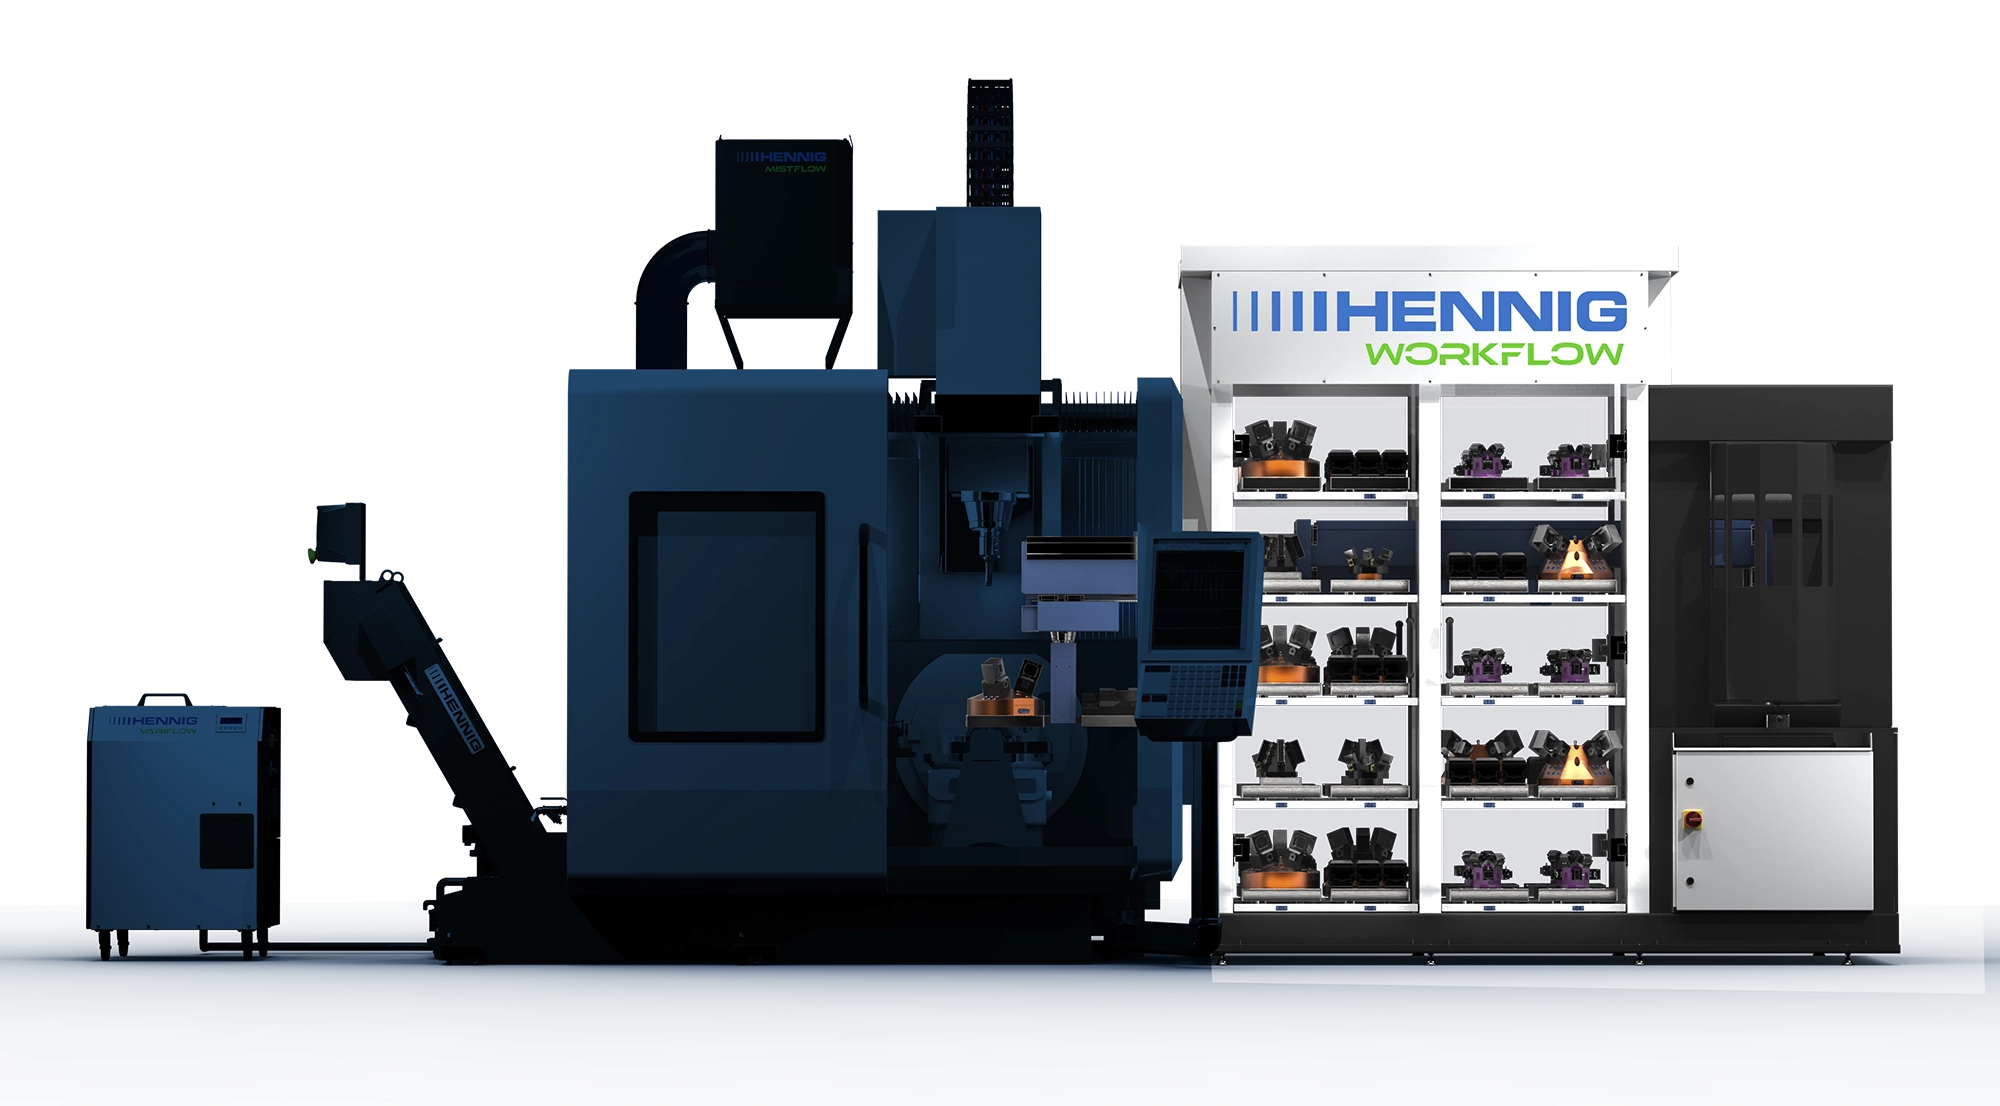
Pallet delivery, robotic tending & software for lights-out production
CNC machining centers, lathes, grinders & multi-axis equipment
Safety systems & rod locks for hydraulic & mechanical presses
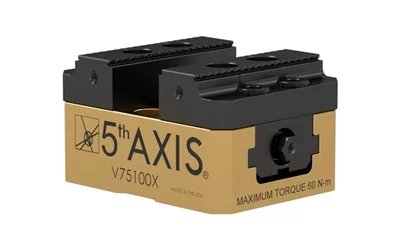
The self-centering CNC machine vise is a game-changer for accuracy, repeatability, and productivity. Designed for a compact footprint with a robust and patented self-centering clamping mechanism, this vise is built for precision and efficiency in high-performance machining.
| Key Features | |
| Self-Centering Technology | Patented self-centering mechanism eliminates time-consuming manual adjustments. |
| Flexible | With 5-inch jaw widths with up to 6-inch open capacity, this vise accommodates a wide range of workpiece shapes and sizes. |
| Precision | Guaranteed micrometer-level precision — this vise is engineered for tight tolerances and repeatability. |
| Quick and Easy Setup | Quick-change design enables fast, secure workpiece loading. |
| Robust Build | Built to withstand challenging environments, the hardened steel body ensures long-lasting durability and reliability. |
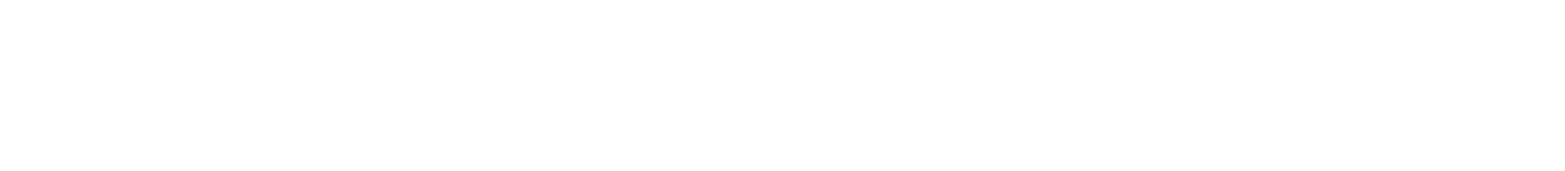
Serrated teeth on each jaw provide maximum grip on stock less than HRC 35. For harder material, the built-in dovetail provides exceptional clamping force with even less torque.
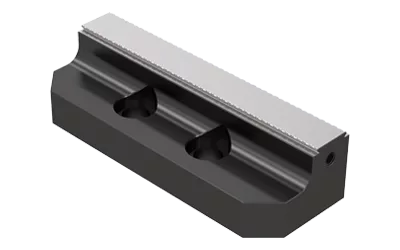
Simply thread in the pull studs and the vise is ready for quick change. Conversely, direct mount any 5th Axis vise from the top down using standard socket head cap screws.
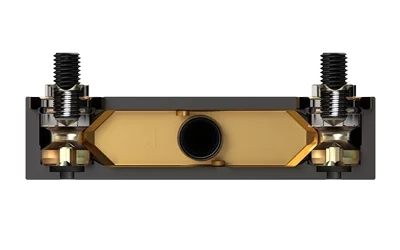
Built from hardened American steel, these jaws can handle any stock type. Vise bases are HRC 32 and vise jaws are HRC 55.
| Product ID | 3D CAD | Mounting Pattern (mm) | Vise Length (mm) | Vise Width (mm) | Vise Height (mm) | Jaw Width | Clamping Force Nm | Max Torque Jaw Bolt | Max Torque Mounting Bolt | Clamping Range Jaws Forward | Clamping Range Jaws Reverse | |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| V75100X | 52 | 100 | 75 | 56.13 | 75 | 22.24 kN at 61.01 Nm | 61.01 | 47.45 | 5.3-43.6 | 47.45 | ||
| V75150X | 52 | 150 | 75 | 56.13 | 75 | 22.24 kN at 61.01 Nm | 61.01 | 47.45 | 5.3-94.1 | 47.45 | ||
| V562X | 96 | 152.4 | 125.73 | 73.64 | 125.73 | 25.13 kN at 74.57 Nm | 74.57 | 47.45 | 8.3-78.0 | 47.45 | ||
| V510X | 96 | 254 | 125.73 | 73.64 | 125.73 | 25.13 kN at 74.57 Nm | 74.57 | 47.45 | 8.3-184.7 | 47.45 |
Each model below is routed to the best next step based on availability.
Every changeover means idle spindle time. Multi-part fixturing slashes setup frequency — so your machines spend more hours cutting and less time waiting.
Based on 250 working days/yr. Multi-part fixturing reduces changeover frequency so your spindle spends more time cutting.
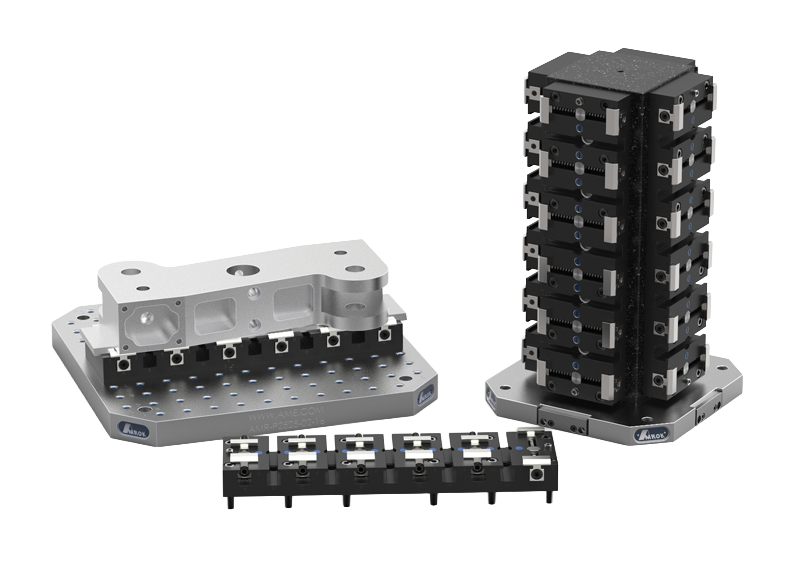
Read our handy guide on how to select the right tombstone from their wide range of products.
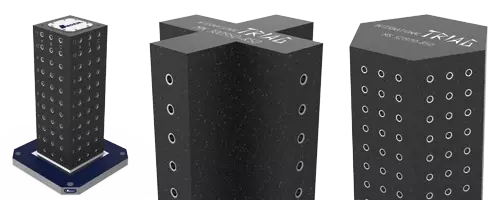
Dr. Tony Schmitz, a professor specializing in vibration analysis, came to AME to do a series of tests on the various material types of tombstones and breaks down his findings to determine the best type of tombstone for your shop.
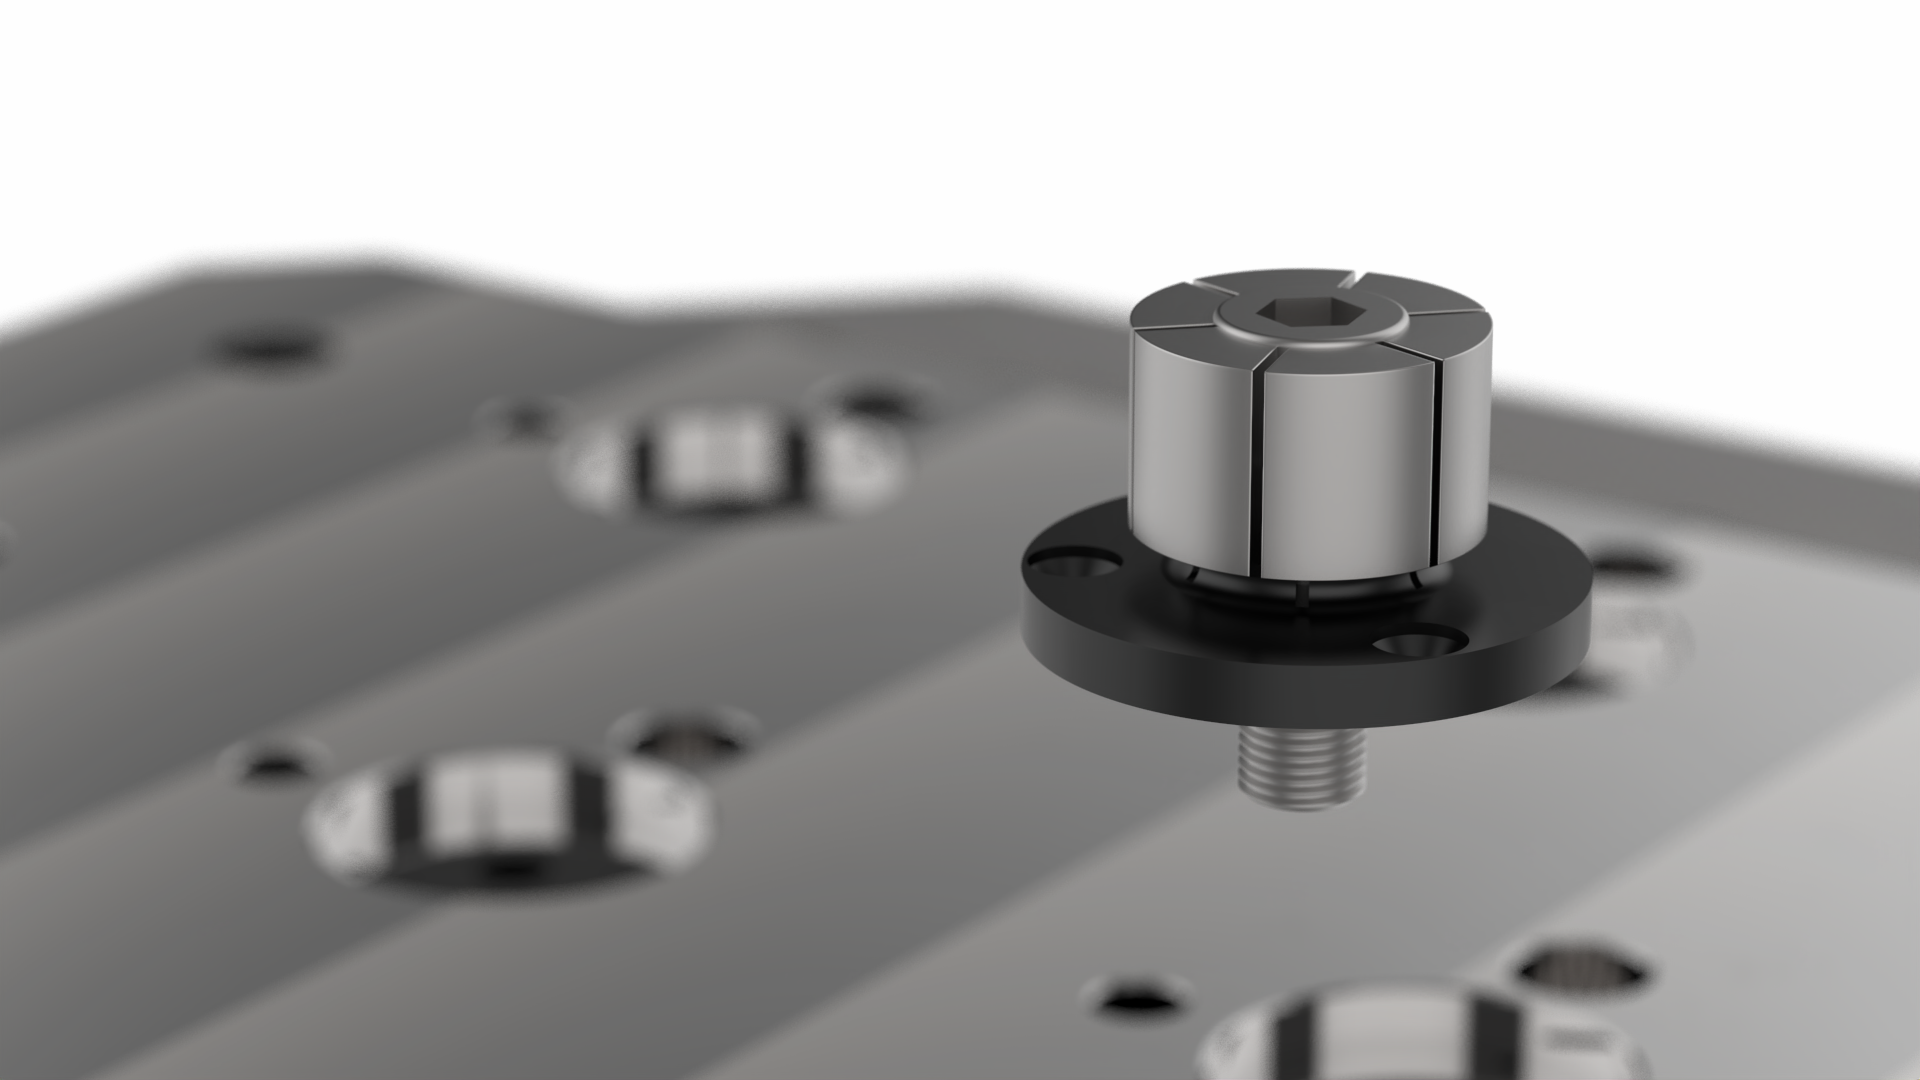
If you want to reduce your overall costs and increase your flexibility to meet your customers’ demands, consider incorporating off-machine set-ups into your machining process.
Both Hennig and its sister company, Advanced Machine & Engineering, now operate under the Hennig brand.
Same team. Same products. Same company. Different look.
Unifying the two brands under one name clarifies our offerings and makes them easier for you to navigate — one website, one team, one trusted partner.