



Blogs
Workholding
Product Selection
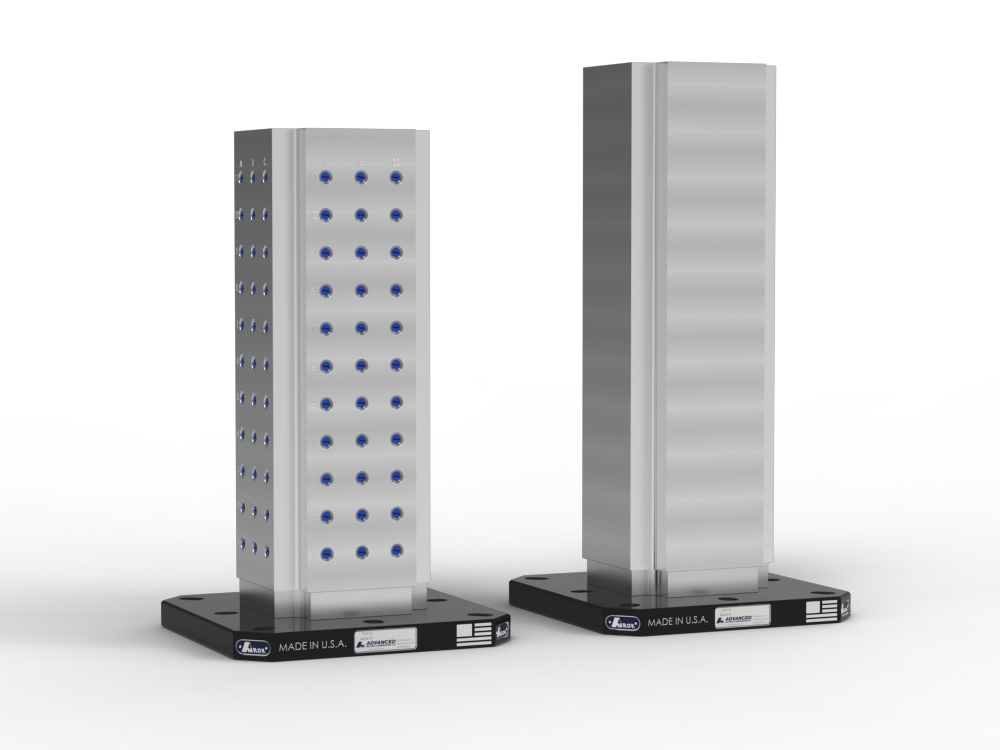
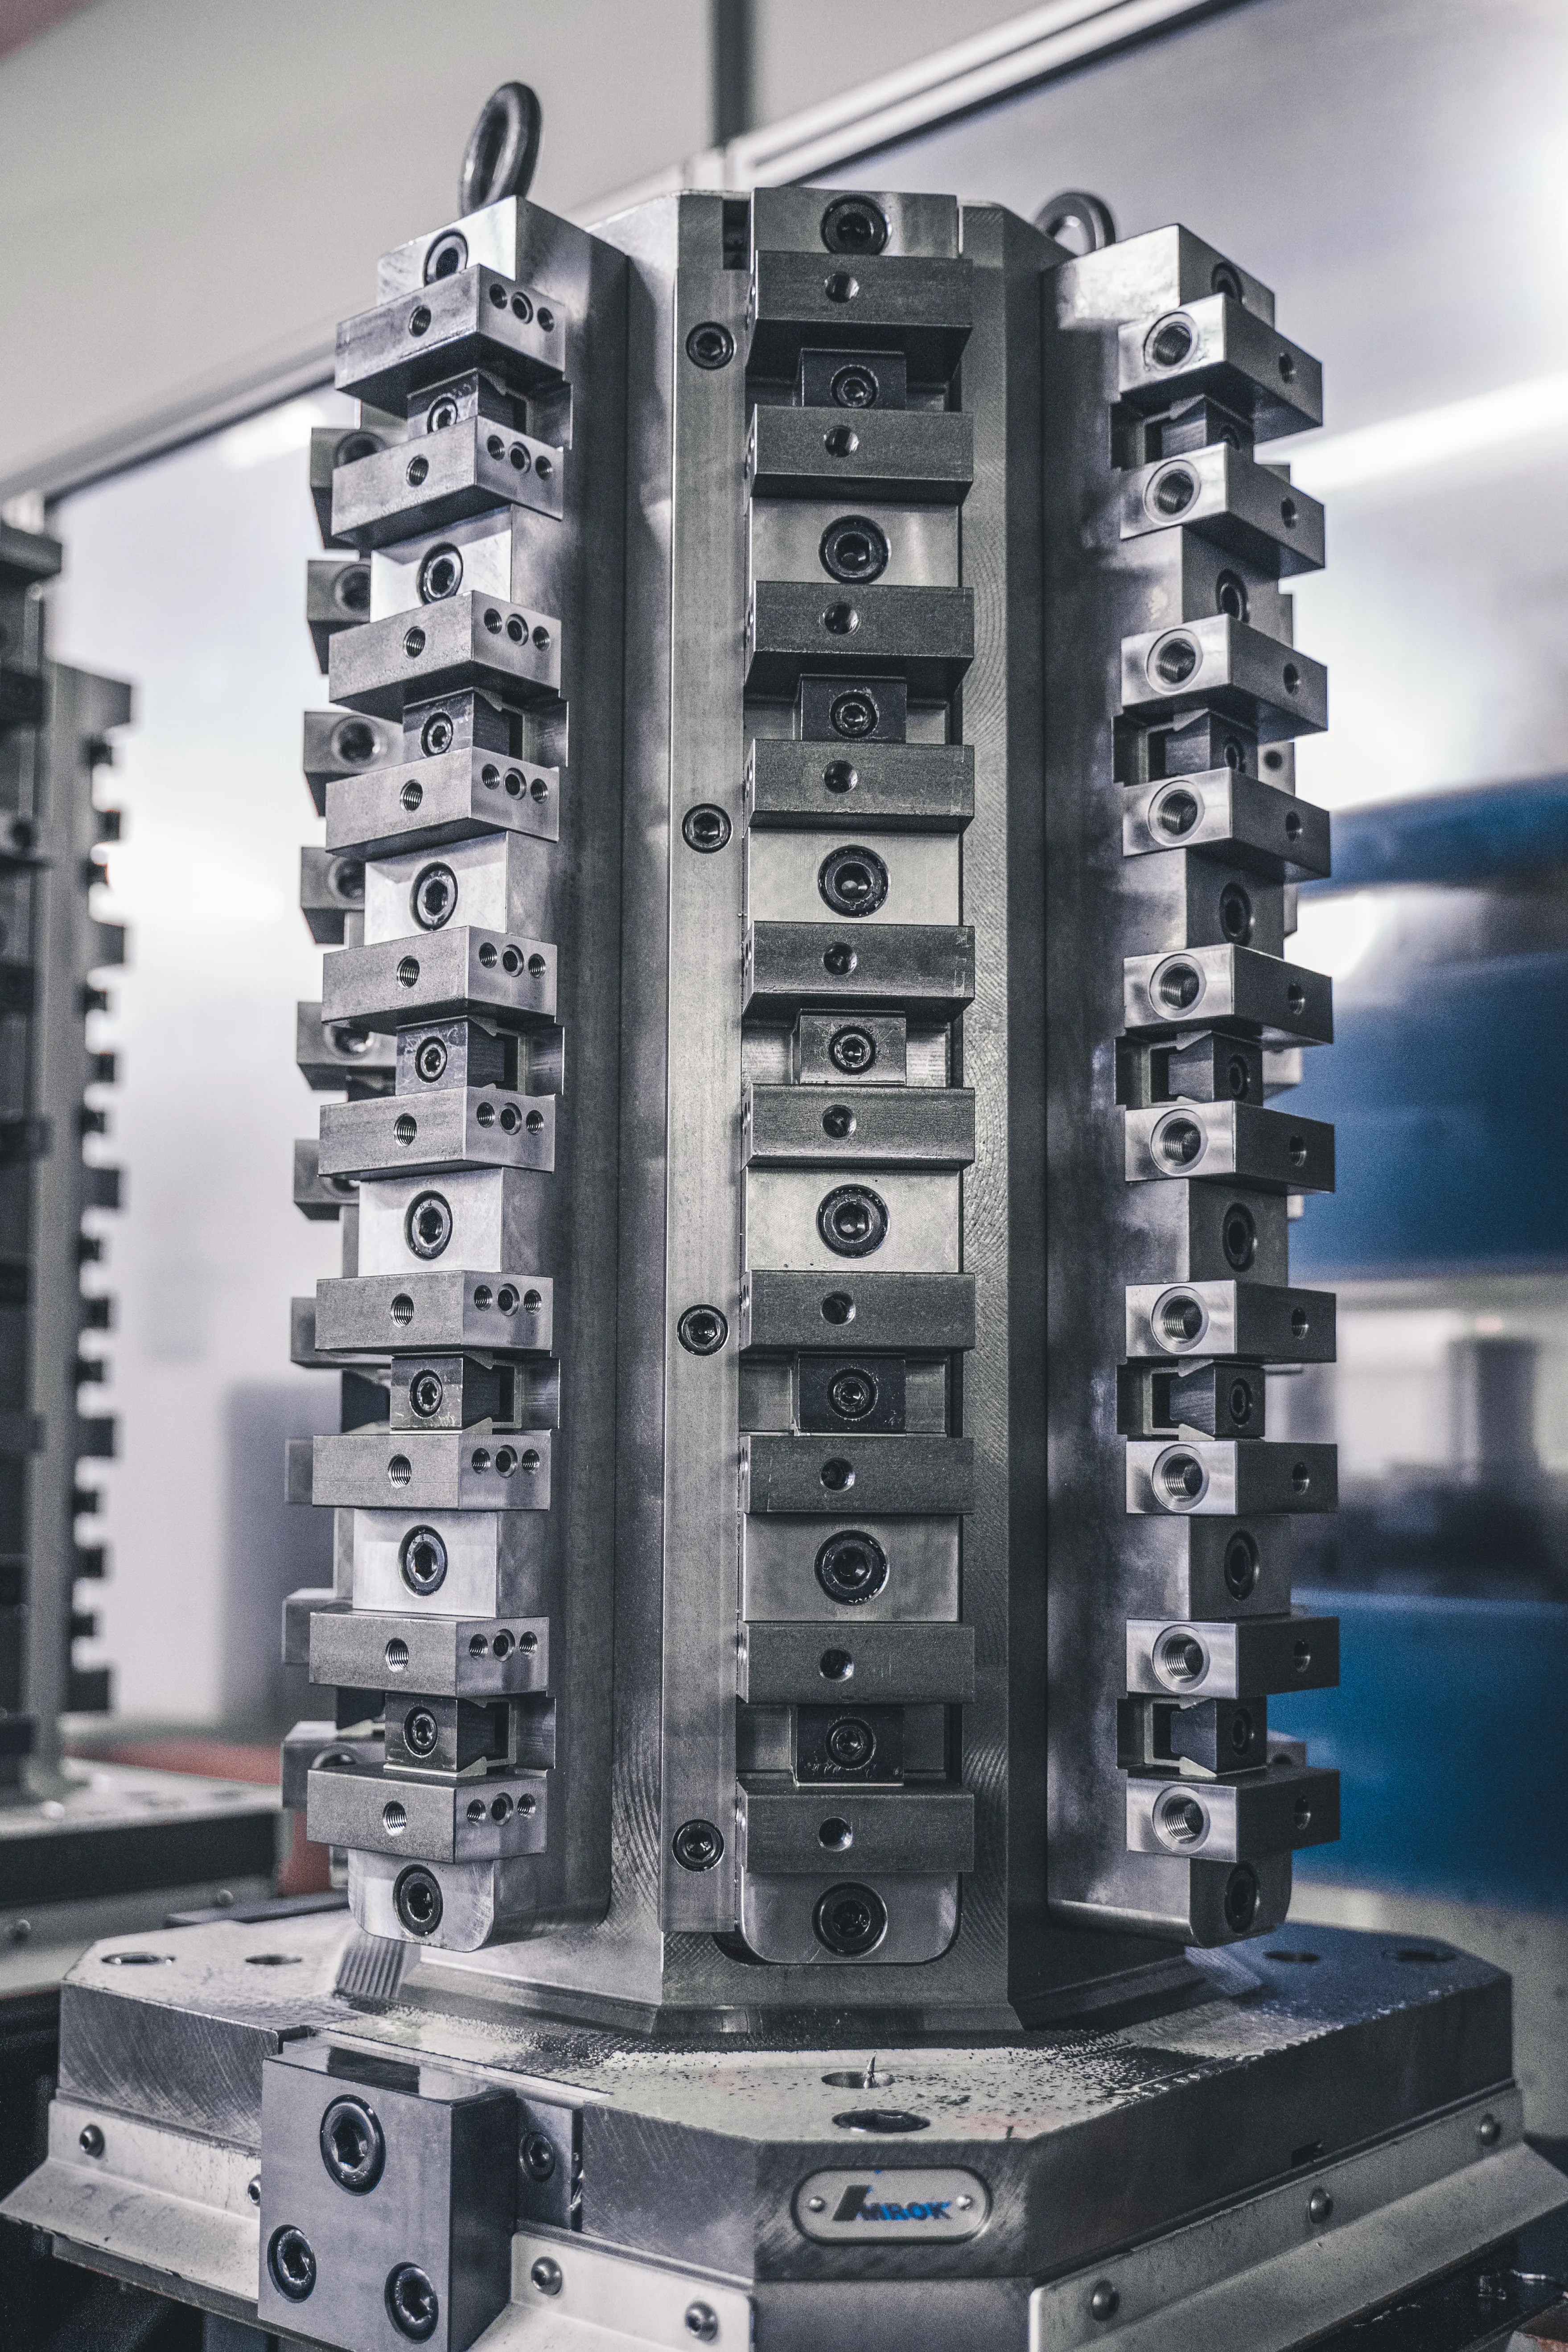
Finding the Right Tombstone is Easy with Hennig
Read our handy guide on how to select the right tombstone from their wide range of products.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.

Hennig Power Protection is a dedicated division specializing in custom-engineered generator enclosures, fuel systems, and power infrastructure for mission-critical applications across data centers, healthcare, telecommunications, and industrial facilities.
Precision machining, fabrication & welding services from our Rockford, IL facility. Complete manufacturing solutions with ISO-certified quality.
Precision machining for turbine...
Pallet delivery, robotic tending & software for lights-out production
CNC machining centers, lathes, grinders & multi-axis equipment
Safety systems & rod locks for hydraulic & mechanical presses
Compact toe clamps are a low-profile solution for high-density machining, delivering exceptional holding force with a small footprint. These clamps pull parts down and in simultaneously, securing the workpiece against the fixture while preserving access to critical surfaces. Ideal for high-speed machining or limited-clearance applications, they help to reduce overall fixture size while increasing spindle uptime. Especially effective when machining flat or low-profile parts in tight configurations, the compact toe clamps are a great fixturing choice.
| Key Features | |
| Low-Profile Hold | Minimal clamp height preserves tool access, z-clearance |
| Wedge-Action Design | Simultaneously pulls the workpiece inward and downward for maximum stability |
| High Clamping Force | Generates up to 12000 lbs of force with simple bolt tightening |
| Versatile Footprint | Fits easily into crowded fixtures or multi-part setups |
| Reusable & Reliable | Hardened components ensure long service life under repeat use |
E – The distance needed between the front of the clamp base and the work piece
I – The distance from the top of the washer to the bottom of the clamp body.
Drill and tap the centerline of “B” for mounting holes.
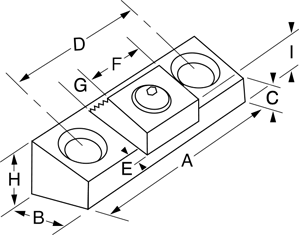
| Product ID | 3D CAD | Units | A | B | C | D | E | F | G | H | I | Total Movement | Mounting Screw | Torque | Holding Force | Replacement Cam Screw | Replacement Square Washer | |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 24106 | Inch | 1.70 in | 0.750 in | 0.50 in | 1.00 in | 0.090 in | 0.75 in | 0.25 in | 0.62 in | 0.845 in | 0.050 in | 5/16-18x3/4 LHCS | 20.8 ft lbs | 2000 lbs | 10370 | 21006 | ||
| 24108 | Inch | 2.12 in | 1.000 in | 0.45 in | 1.32 in | 0.110 in | 1.00 in | 0.38 in | 0.62 in | 0.96 in | 0.100 in | 3/8-16x3/4 LHCS | 65.0 ft lbs | 4000 lbs | 10372 | 21016 | ||
| 24110 | Inch | 2.95 in | 1.500 in | 0.99 in | 2.00 in | 0.130 in | 1.50 in | 0.50 in | 1.25 in | 1.700 in | 0.100 in | 1/2-13x11/4 SHCS | 100.0 ft lbs | 6000 lbs | 10376 | 21026 | ||
| 54110 | Metric | 43.2 mm | 19.0 mm | 12.7 mm | 25.4 mm | 2.3 mm | 19.0 mm | 6.4 mm | 15.75 mm | 21.5 mm | 1.2 mm | M8x16 LHCS | 28 nM | 8900 N | 50368 | 21006 | ||
| 54112 | Metric | 54.0 mm | 25.4 mm | 11.4 mm | 33.5 mm | 2.8 mm | 25.4 mm | 9.7 mm | 15.75 mm | 24.4 mm | 2.0 mm | M10x20 LHCS | 88 nM | 17800 N | 50372 | 51016 | ||
| 54116 | Metric | 75.0 mm | 38.1 mm | 25.2 mm | 50.8 mm | 3.3 mm | 38.1 mm | 12.7 mm | 31.75 mm | 43.2 mm | 2.5 mm | M12x30 SHCS | 136 nM | 26700 N | 51016 | 21026 |
Each model below is routed to the best next step based on availability.
Every changeover means idle spindle time. Multi-part fixturing slashes setup frequency — so your machines spend more hours cutting and less time waiting.
Based on 250 working days/yr. Multi-part fixturing reduces changeover frequency so your spindle spends more time cutting.
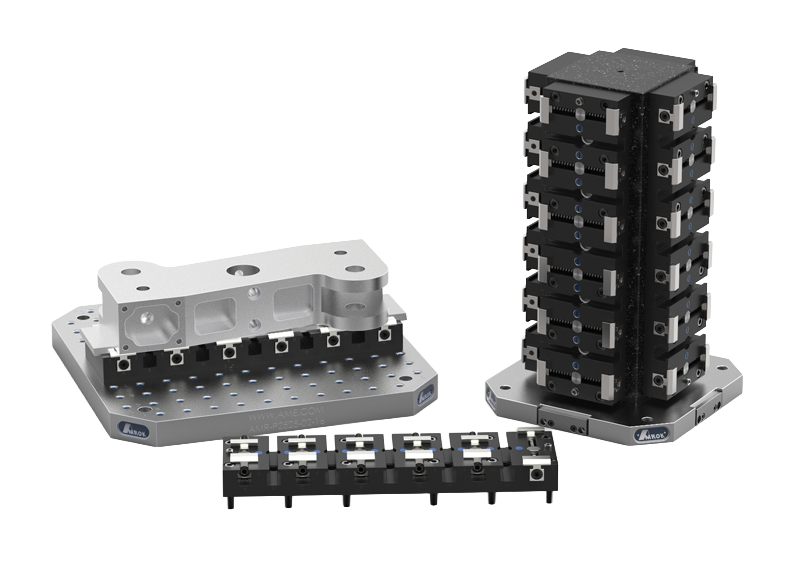
Read our handy guide on how to select the right tombstone from their wide range of products.
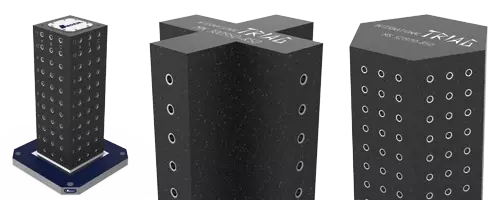
Dr. Tony Schmitz, a professor specializing in vibration analysis, came to AME to do a series of tests on the various material types of tombstones and breaks down his findings to determine the best type of tombstone for your shop.
If you want to reduce your overall costs and increase your flexibility to meet your customers’ demands, consider incorporating off-machine set-ups into your machining process.
Both Hennig and its sister company, Advanced Machine & Engineering, now operate under the Hennig brand.
Same team. Same products. Same company. Different look.
Unifying the two brands under one name clarifies our offerings and makes them easier for you to navigate — one website, one team, one trusted partner.