



Blogs
Workholding
Product Selection
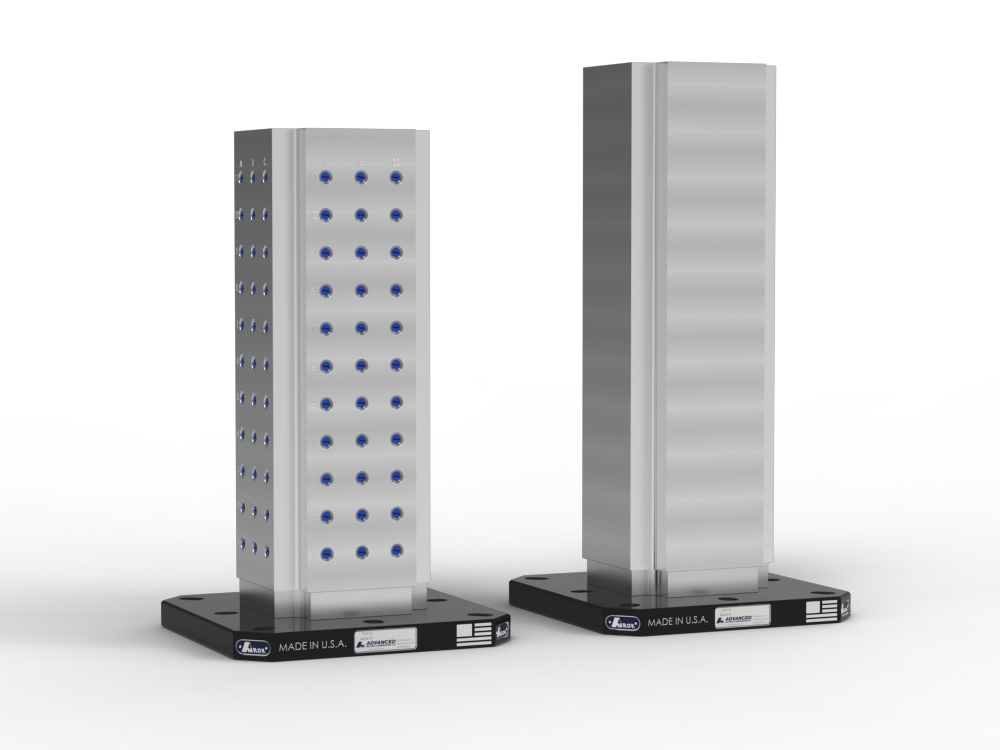
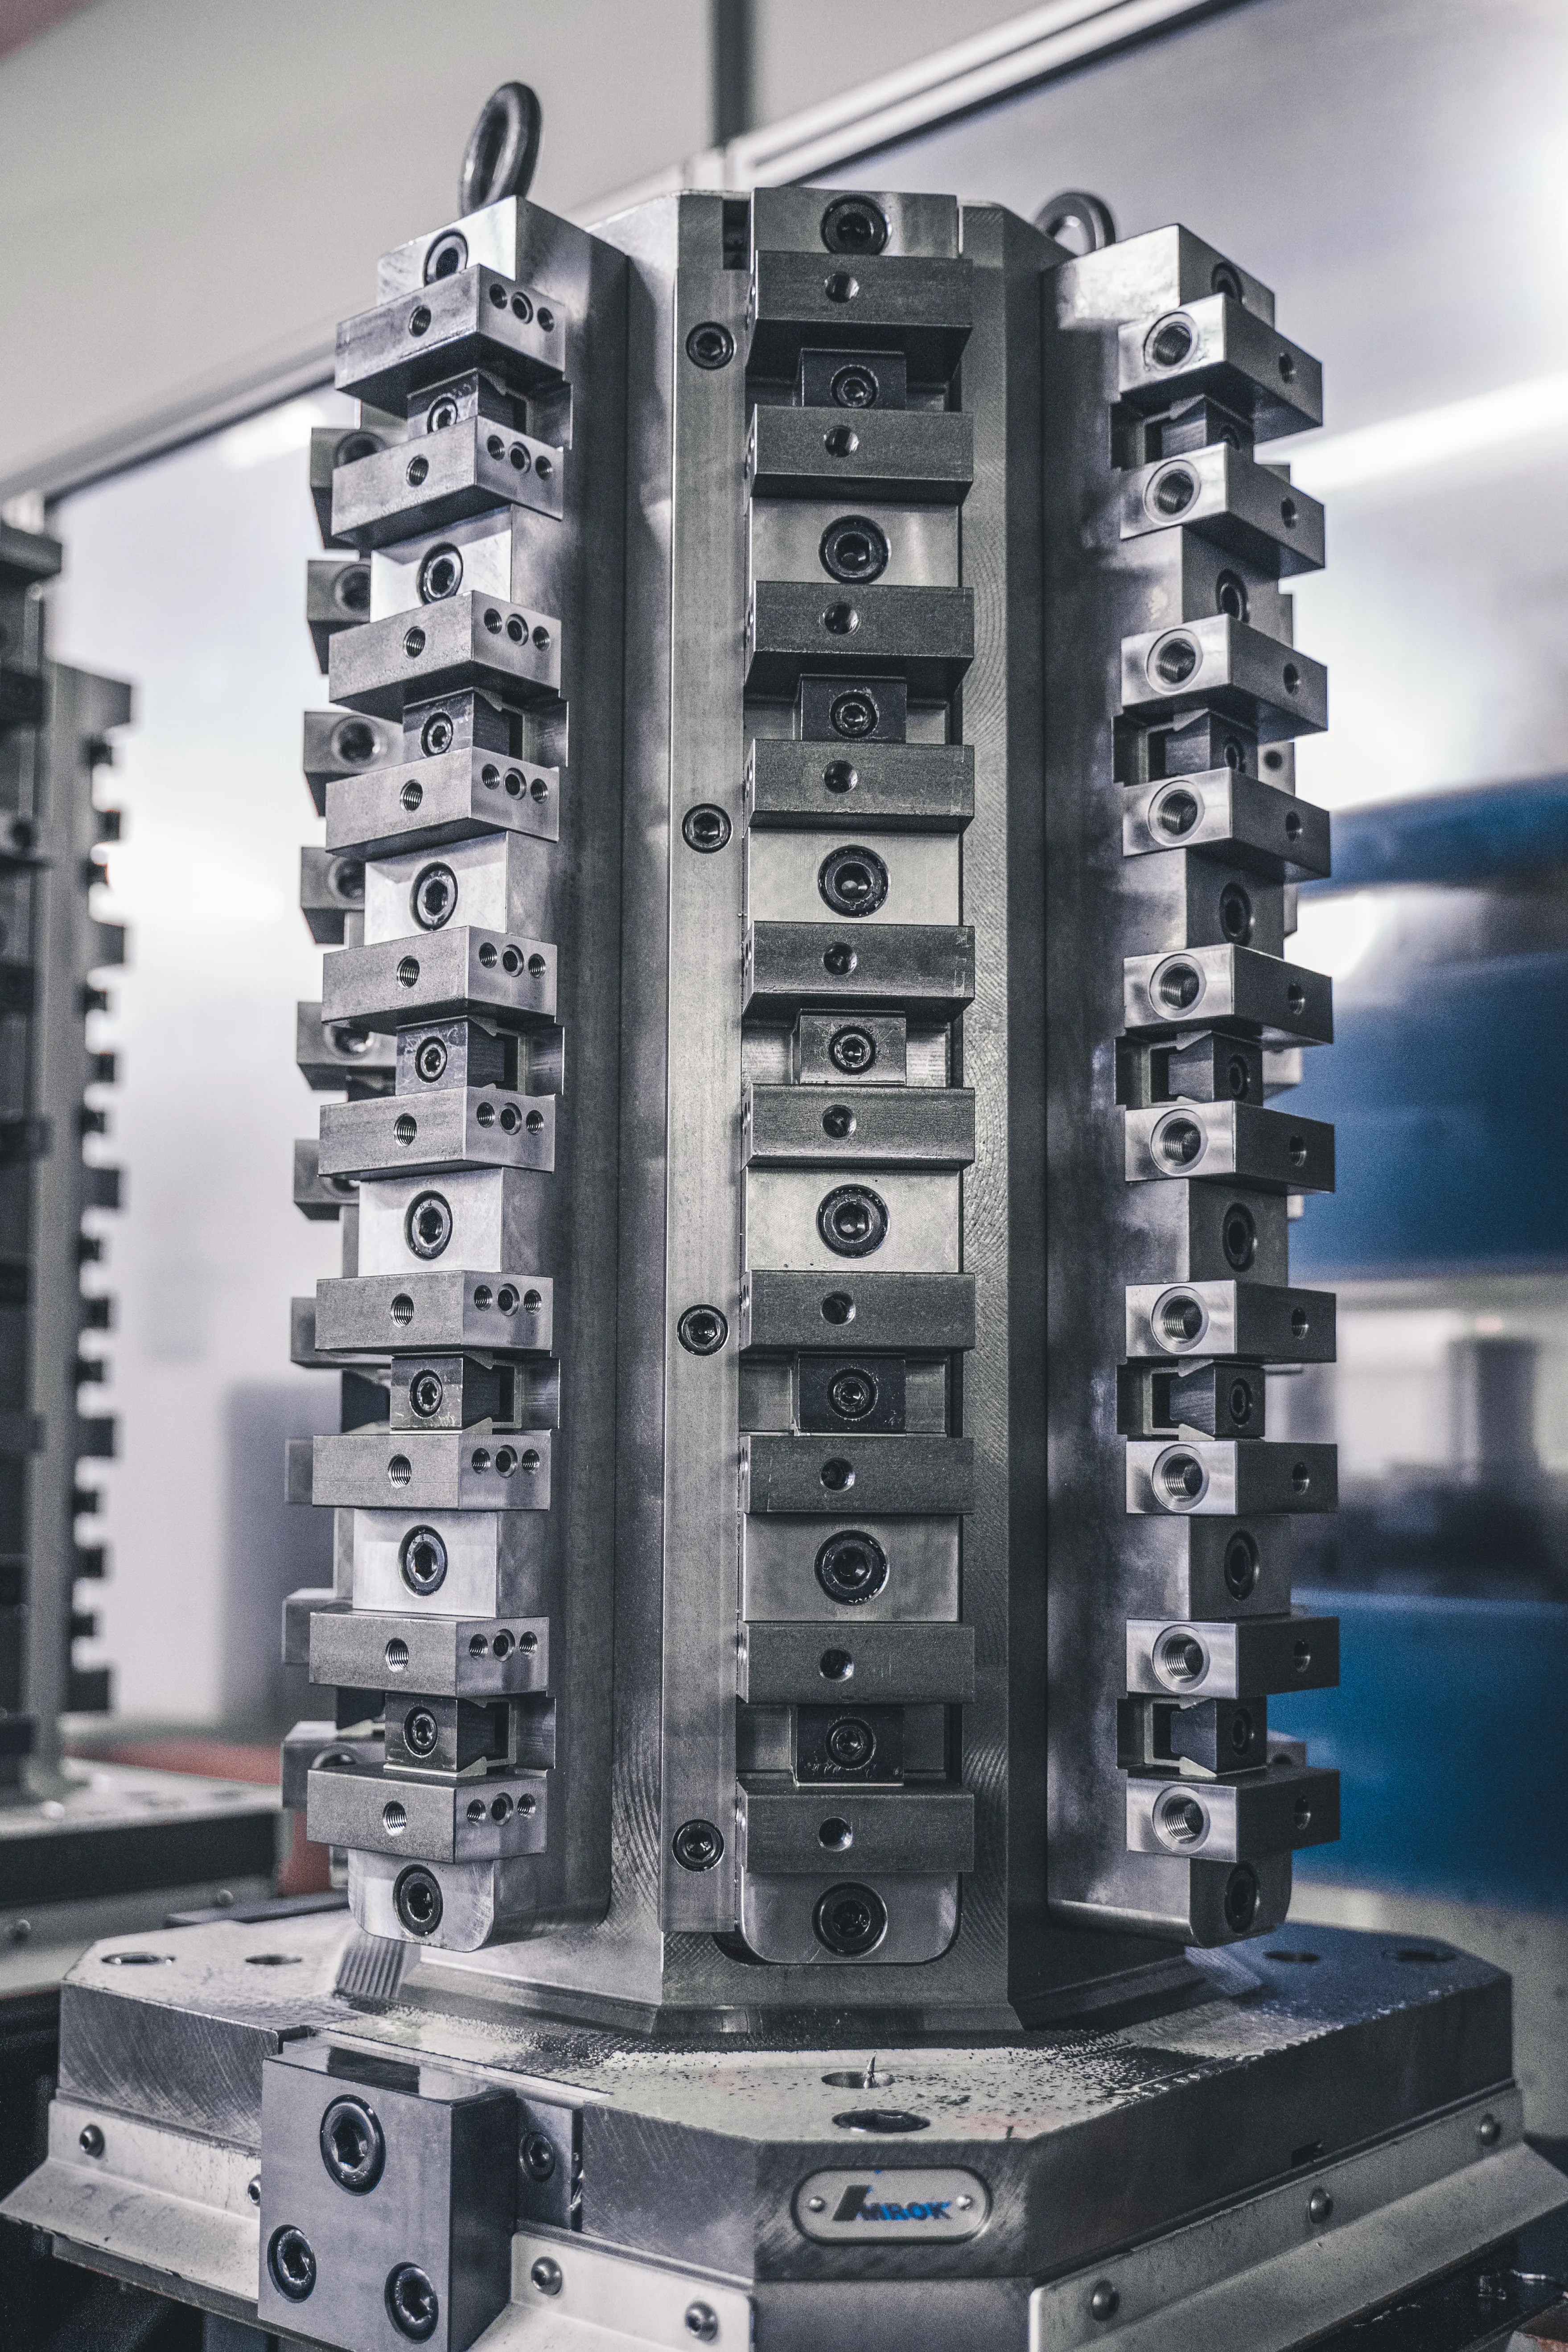
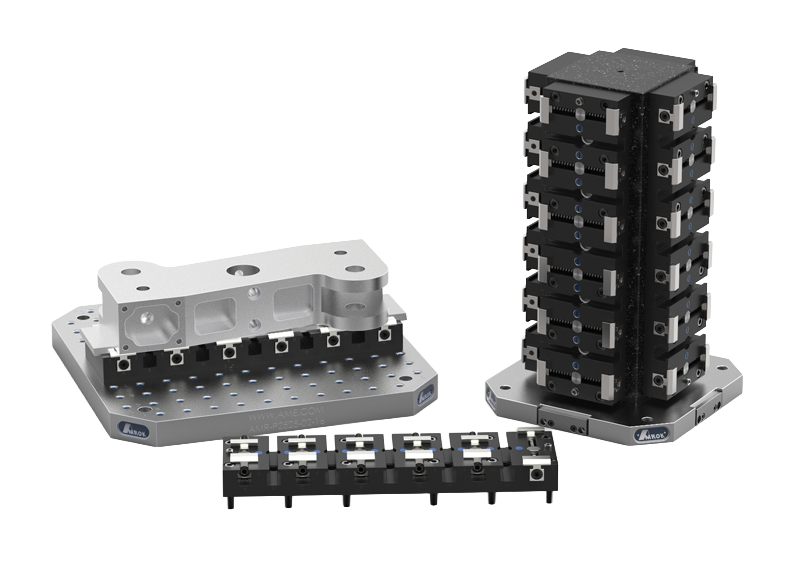
Finding the Right Tombstone is Easy with Hennig
Read our handy guide on how to select the right tombstone from their wide range of products.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.

Hennig Power Protection is a dedicated division specializing in custom-engineered generator enclosures, fuel systems, and power infrastructure for mission-critical applications across data centers, healthcare, telecommunications, and industrial facilities.
Precision machining, fabrication & welding services from our Rockford, IL facility. Complete manufacturing solutions with ISO-certified quality.
Precision machining for turbine...
Pallet delivery, robotic tending & software for lights-out production
CNC machining centers, lathes, grinders & multi-axis equipment
Safety systems & rod locks for hydraulic & mechanical presses
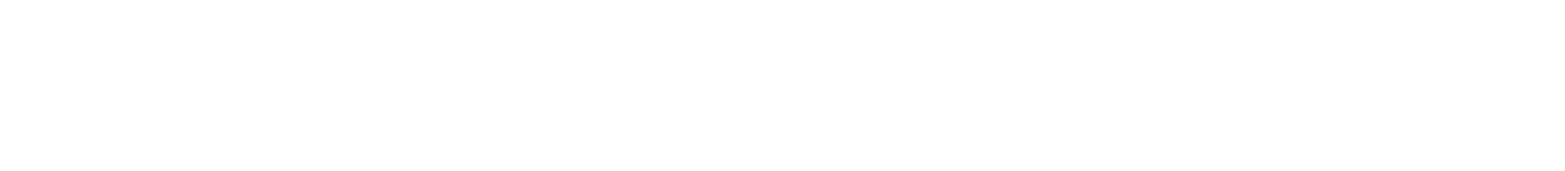
Dyna-Force® clamps use a unique cam mechanism to apply consistent lateral pressure while keeping the top of the part clear for machining. These clamps provide uniform holding force regardless of part size variation and are excellent for clamping castings, thin-walled components, or soft materials were downward pressure might distort the part. Their modular base design allows for precise positioning along fixture rails or plates.
| Key Features | |
| Edge-Only Clamping | Keeps top of part accessible for full-surface machining |
| Consistent Force Output | Independent of part size or variation |
| Modular Base | Easily repositions along standard fixture rails |
| Low Distortion | Ideal for thin or flexible parts that deform under vertical pressure |
| Repetitive Accuracy | Maintains consistent hold across batches |
Notes:
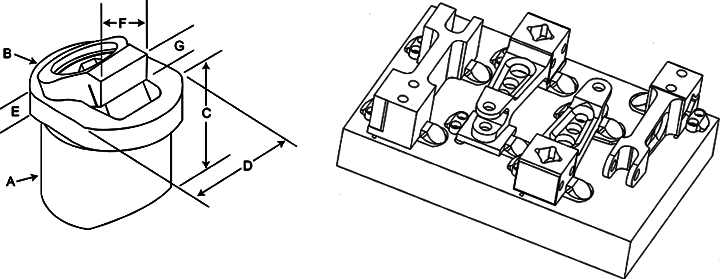
| Product ID | 3D CAD | Clamp Jaw Hardness | A** (in) | B (in) | C (in) | D (in) | E (in) | F (in) | G Min | G Optimal | G Max | Clamp Travel | Drive Screw | Key Size | Torque Max Ftlbs | Holding Force Lbs | Replacement Clamp Jaw Inserts | |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 28314 | Smooth 34RC | 20.00 | 24.90 | 19.00 | 19.90 | 4.50 | 13.50 | 3.250 | 5.000 | 6.750 | 2.0 | M6x12mm SHCS | 5 | 7.3 ft lbs (9.9 Nm) | 2000 lbs (9986 N) | 28480 (20mm smooth) | ||
| 28318 | Serrated 44RC | 20.00 | 24.90 | 19.00 | 19.90 | 4.50 | 13.50 | 3.250 | 5.000 | 6.750 | 2.0 | M6x12mm SHCS | 5 | 7.3 ft lbs (9.9 Nm) | 2000 lbs (9986 N) | 28482 (20mm serrated) | ||
| 28320 | Smooth 34RC | 25.00 | 29.90 | 24.00 | 24.90 | 5.00 | 15.00 | 4.500 | 6.500 | 8.250 | 2.2 | M8x16mm SHCS | 6 | 17.6 ft lbs (23.9 Nm) | 2600 lbs (11565 N) | 28484 (25mm smooth) | ||
| 28322 | Serrated 44RC | 25.00 | 29.90 | 24.00 | 24.90 | 5.00 | 15.00 | 4.500 | 6.500 | 8.250 | 2.2 | M8x16mm SHCS | 6 | 17.6 ft lbs (23.9 Nm) | 2600 lbs (11565 N) | 28486 (25mm serrated) | ||
| 28324 | Smooth 34RC | 30.00 | 37.90 | 29.00 | 29.90 | 7.00 | 20.00 | 4.500 | 7.500 | 10.750 | 3.8 | M10x18mm SHCS | 8 | 35.3 ft lbs (41.9 Nm) | 3200 lbs (14234 N) | 28488 (30mm smooth) | ||
| 28328 | Serrated 44RC | 30.00 | 37.90 | 29.00 | 29.90 | 7.00 | 20.00 | 4.500 | 7.500 | 10.750 | 3.8 | M10x18mm SHCS | 8 | 35.3 ft lbs (41.9 Nm) | 3200 lbs (14234 N) | 28490 (30mm serrated) |
Each model below is routed to the best next step based on availability.
Every changeover means idle spindle time. Multi-part fixturing slashes setup frequency — so your machines spend more hours cutting and less time waiting.
Based on 250 working days/yr. Multi-part fixturing reduces changeover frequency so your spindle spends more time cutting.
Read our handy guide on how to select the right tombstone from their wide range of products.
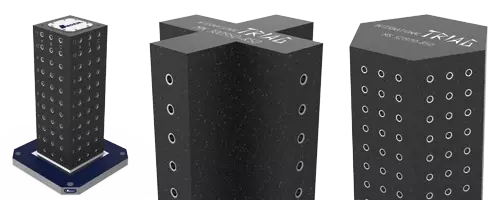
Dr. Tony Schmitz, a professor specializing in vibration analysis, came to AME to do a series of tests on the various material types of tombstones and breaks down his findings to determine the best type of tombstone for your shop.
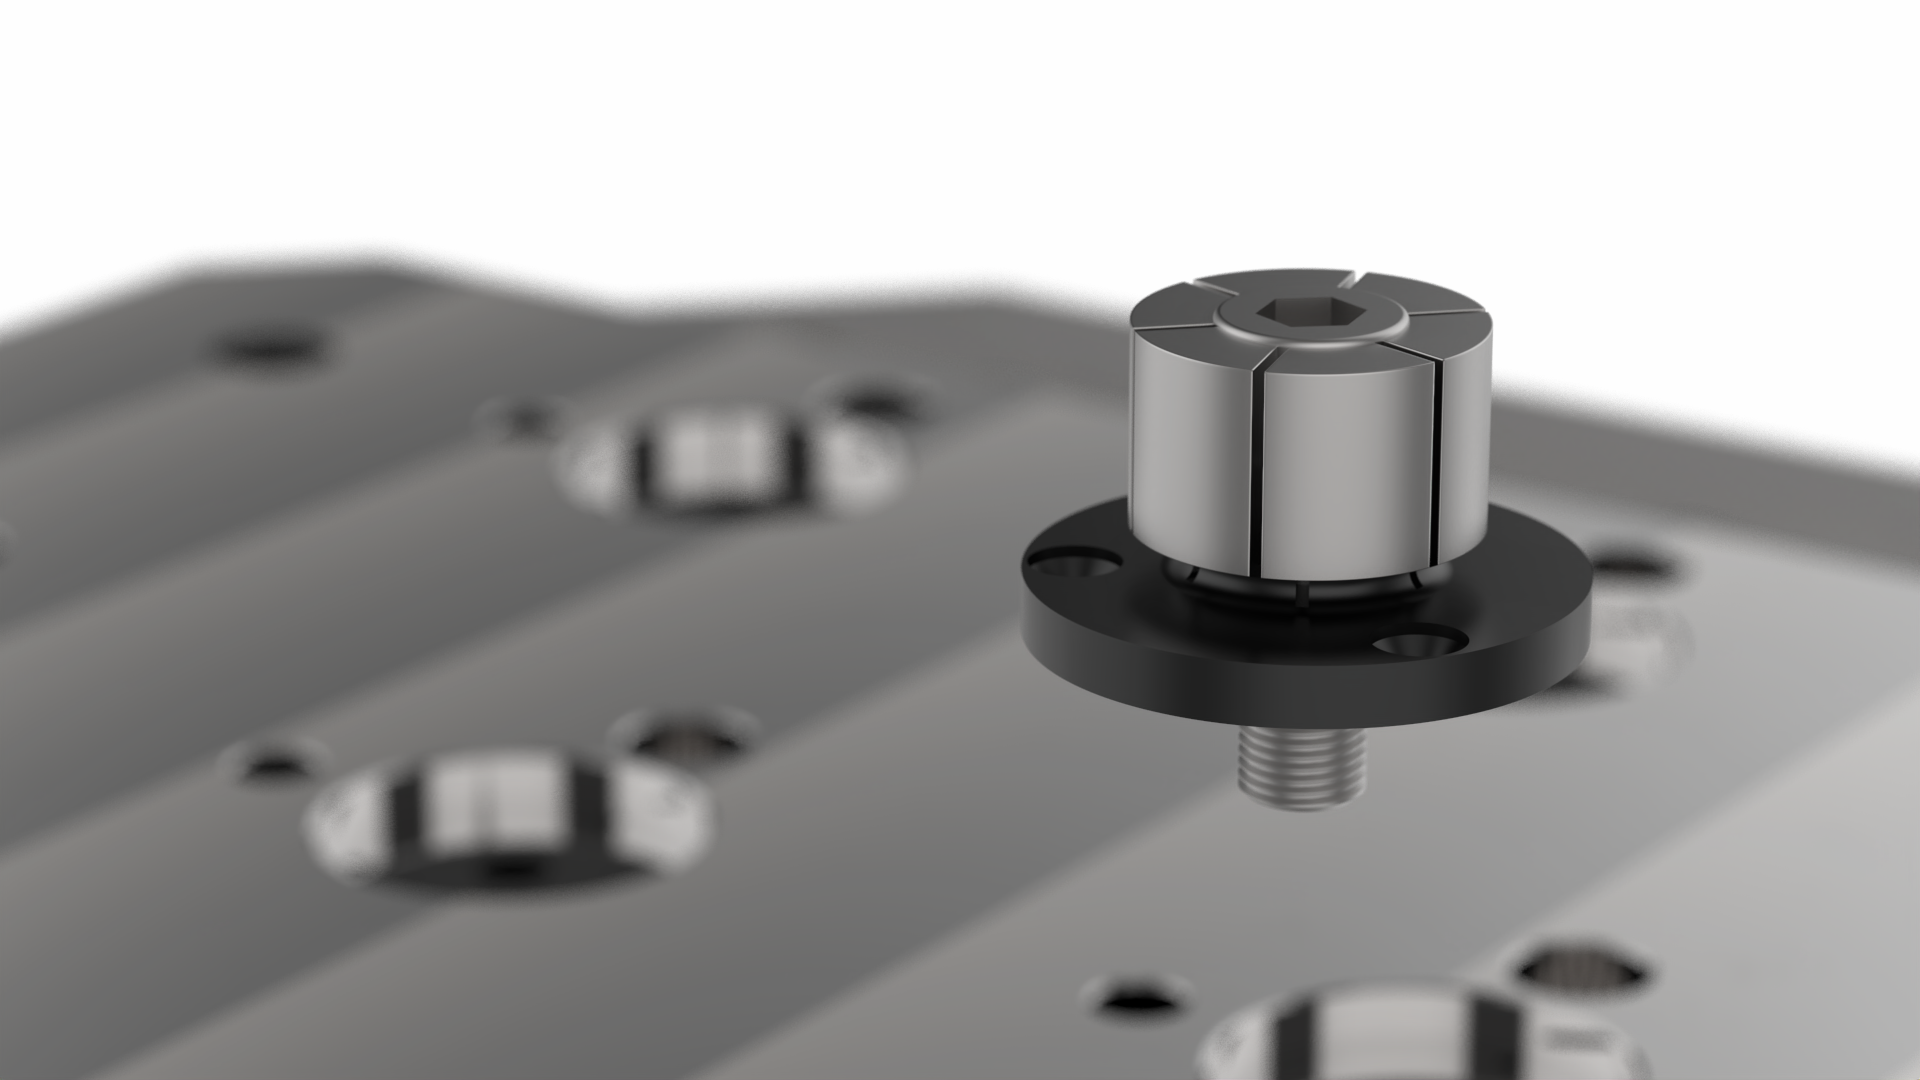
If you want to reduce your overall costs and increase your flexibility to meet your customers’ demands, consider incorporating off-machine set-ups into your machining process.
Both Hennig and its sister company, Advanced Machine & Engineering, now operate under the Hennig brand.
Same team. Same products. Same company. Different look.
Unifying the two brands under one name clarifies our offerings and makes them easier for you to navigate — one website, one team, one trusted partner.