



Blogs
Workholding
Product Selection
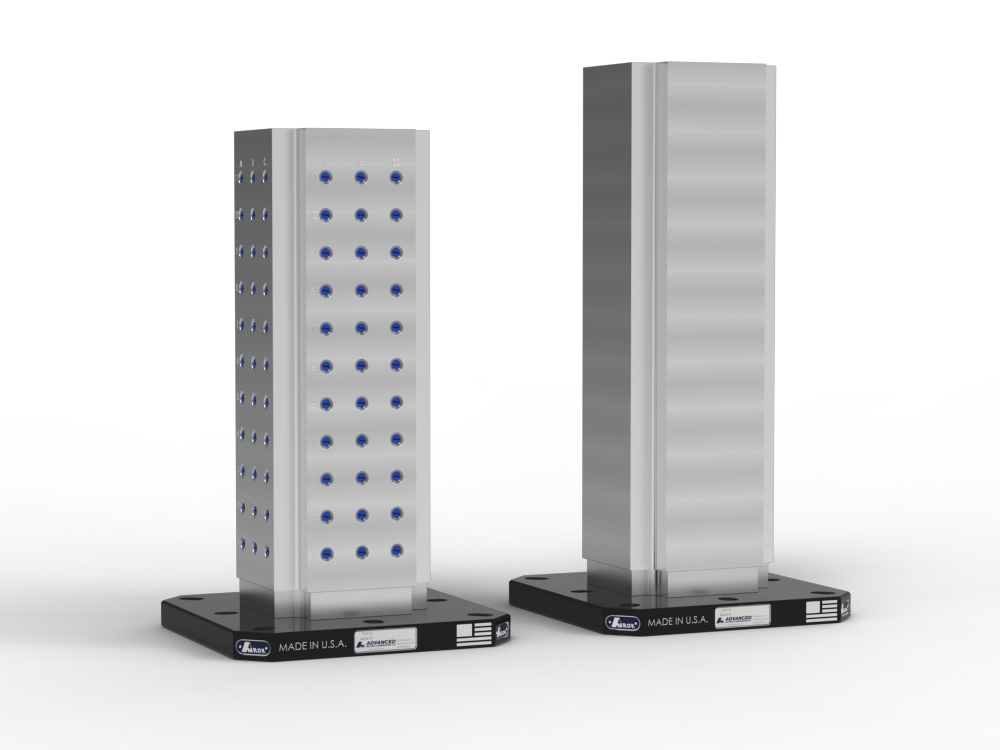
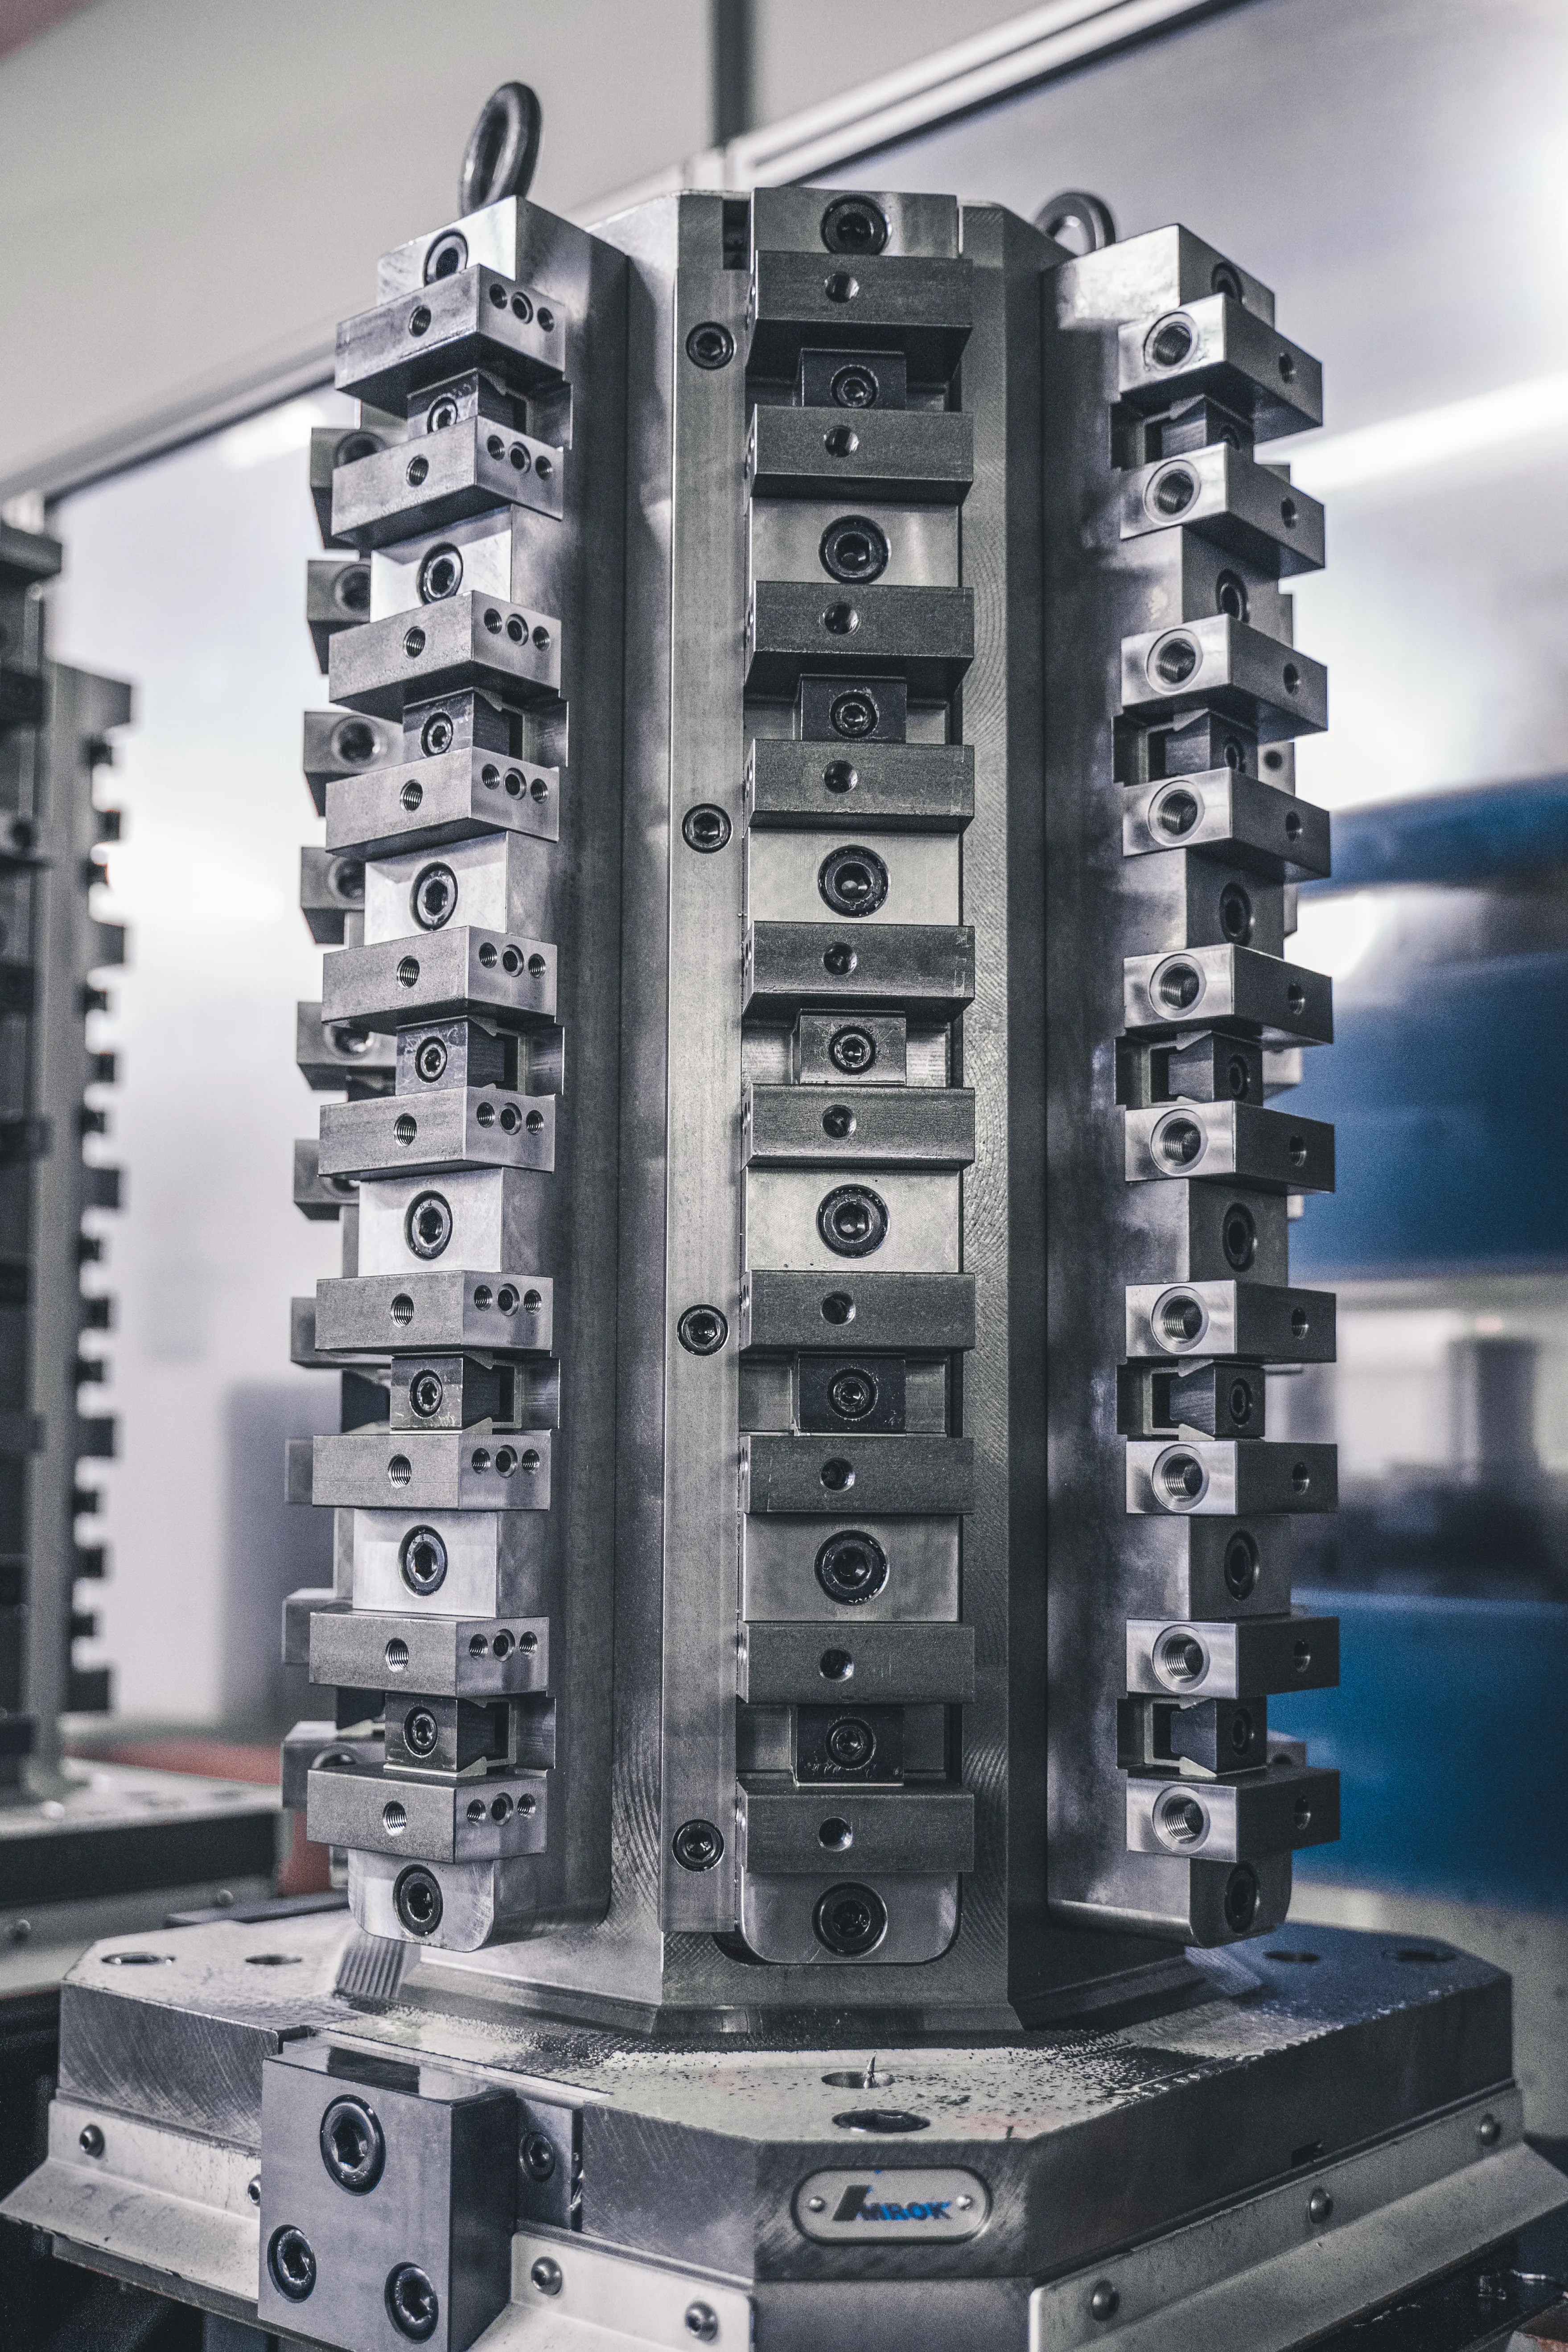
Finding the Right Tombstone is Easy with Hennig
Read our handy guide on how to select the right tombstone from their wide range of products.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.
Download installation and maintenance manuals, order spare parts, and find tutorial videos to help with your chip conveyor installation and operation.

Hennig Power Protection is a dedicated division specializing in custom-engineered generator enclosures, fuel systems, and power infrastructure for mission-critical applications across data centers, healthcare, telecommunications, and industrial facilities.
Precision machining, fabrication & welding services from our Rockford, IL facility. Complete manufacturing solutions with ISO-certified quality.
Precision machining for turbine...
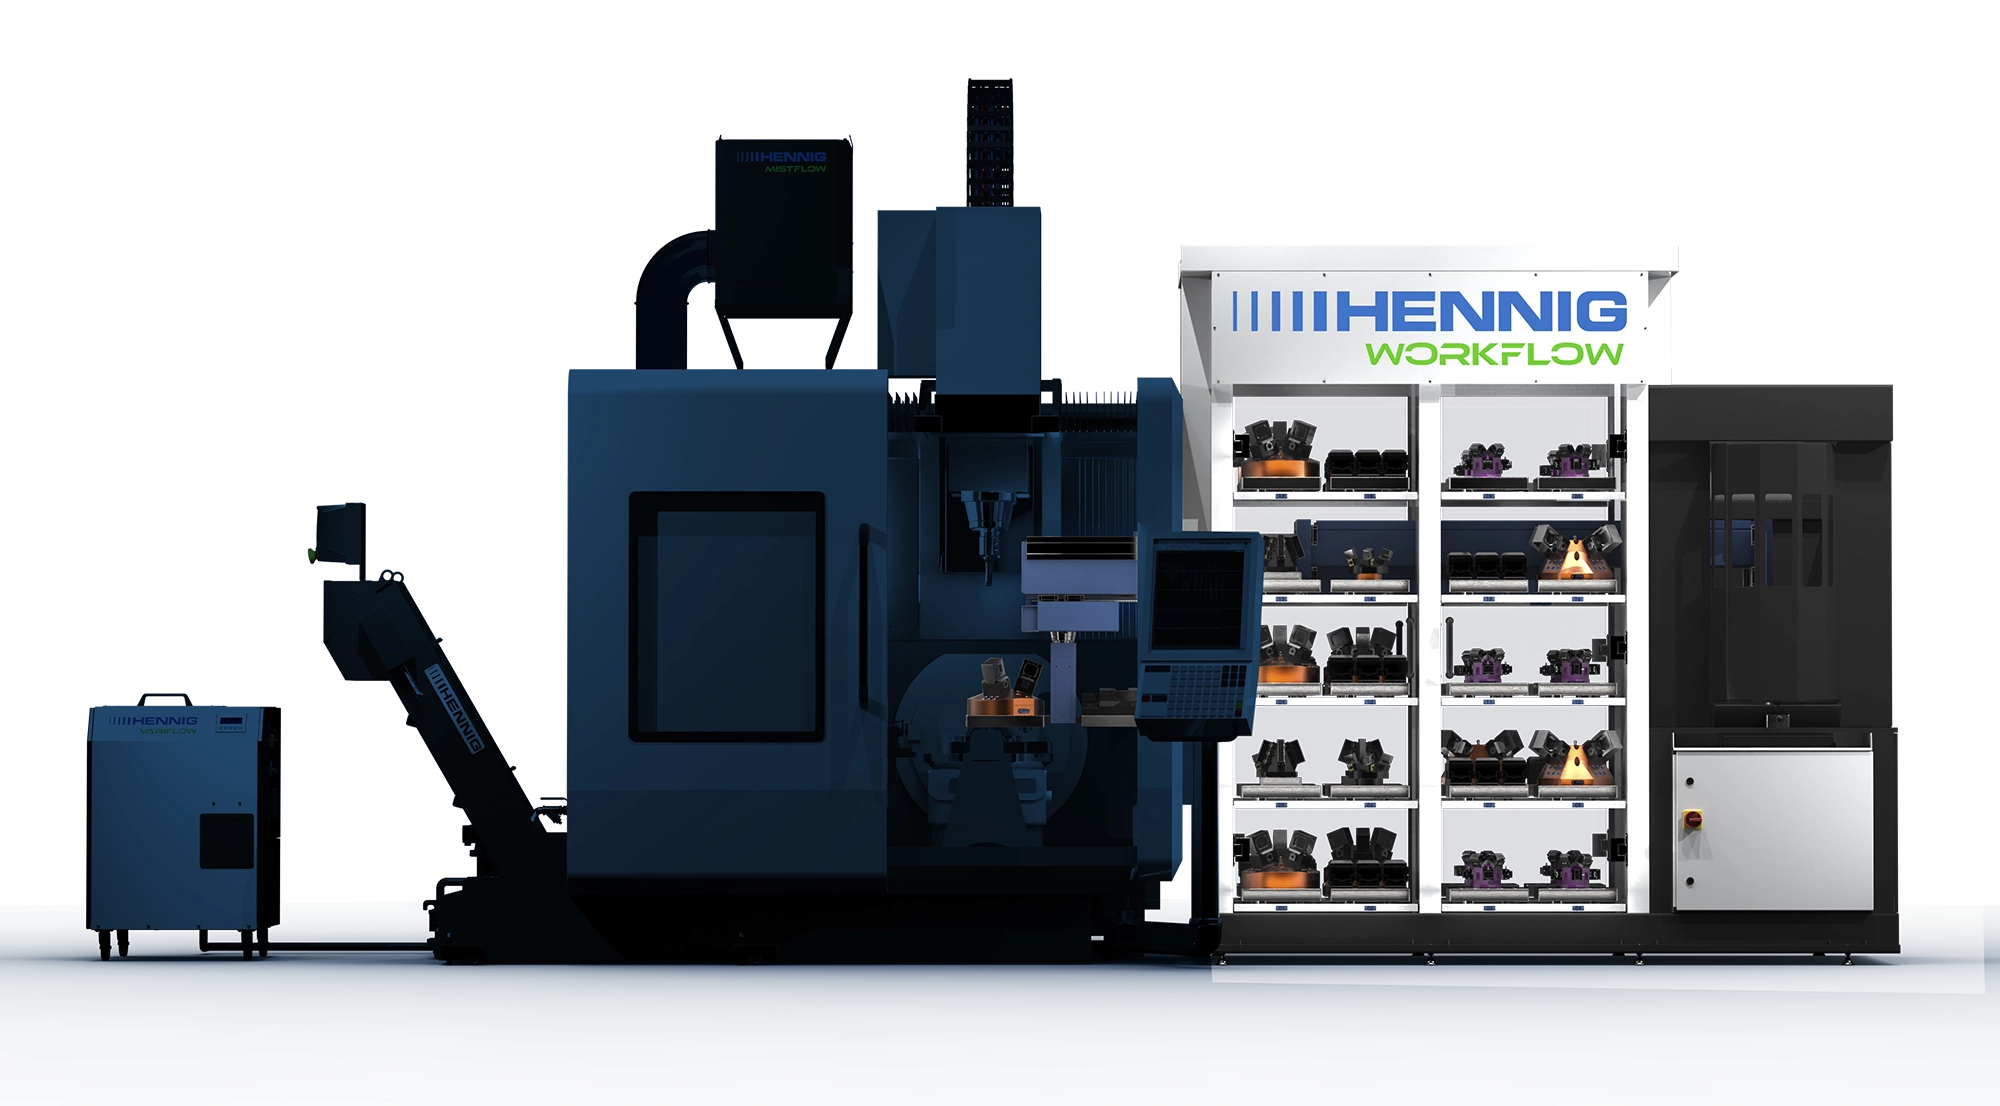
Pallet delivery, robotic tending & software for lights-out production
CNC machining centers, lathes, grinders & multi-axis equipment
Safety systems & rod locks for hydraulic & mechanical presses
The SCHUNK KNOTEC KSC-D is a dual-station vise (or double vise) engineered for machining multiple parts on one setup. With a patented "third-hand" function that securely holds the first workpiece while the second hand is actuated, this vise is a total standout. This vise's extremely flat design and light weight make it ideal for automation setups including locading and high-volume production.
| Key Features | |
| Third-Hand Function | Innovatively holds two workpieces independently; load the first part and it will stay clamped with spring tension while the other part is positioned |
| Low-Profile | Extremely flat build, maximizing vertical space and minimizing deflection |
| Rigid Construction | Clamping is done by tension/pull-down rather than push, preventing base body bending even under high forces |
| High Clamping Forces & Reliability | Each station supplies strong clamping force for secure machining applications; low-maintenance operation enabled by encapsulated spindle and base jaws |
| VERO-S Quick-Change Interface | Comes ready to integrate with SCHUNK's VERO-S zero-point system, drastically reducing changeover time in automated cells |
| Available Accessories | Compatible with the broader KSC family of jaws and accessories |
| Product ID | 3D CAD | Part Number | Width Of Clamping Vise | Vise Length | Version | |
|---|---|---|---|---|---|---|
| KSC-D 80-300 | 1322945 | 80.0 mm | 300.0 mm | - | ||
| KSC-D 125-320 | 1322939 | 125.0 mm | 320.0 mm | - | ||
| KSC-D 125-390 | 1334720 | 125.0 mm | 390.0 mm | - | ||
| KSC-D 125-460 | 1334721 | 125.0 mm | 460.0 mm | - | ||
| KSC-D 125-530 | 1334722 | 125.0 mm | 530.0 mm | - | ||
| KSC-D 125-600 | 1334723 | 125.0 mm | 600.0 mm | - | ||
| KSC-D 125-670 | 1334724 | 125.0 mm | 670.0 mm | - | ||
| KSC-D 125-740 | 1322940 | 125.0 mm | 740.0 mm | - |
Each model below is routed to the best next step based on availability.
Every changeover means idle spindle time. Multi-part fixturing slashes setup frequency — so your machines spend more hours cutting and less time waiting.
Based on 250 working days/yr. Multi-part fixturing reduces changeover frequency so your spindle spends more time cutting.
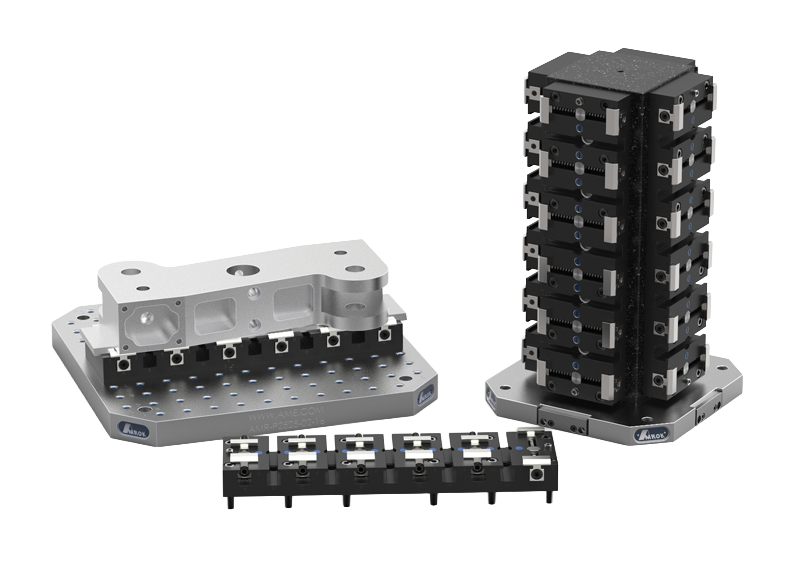
Read our handy guide on how to select the right tombstone from their wide range of products.
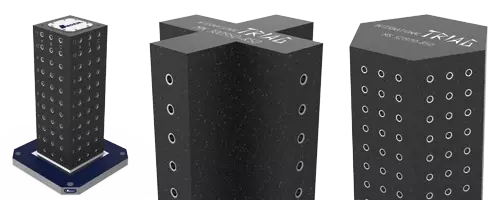
Dr. Tony Schmitz, a professor specializing in vibration analysis, came to AME to do a series of tests on the various material types of tombstones and breaks down his findings to determine the best type of tombstone for your shop.
If you want to reduce your overall costs and increase your flexibility to meet your customers’ demands, consider incorporating off-machine set-ups into your machining process.
Both Hennig and its sister company, Advanced Machine & Engineering, now operate under the Hennig brand.
Same team. Same products. Same company. Different look.
Unifying the two brands under one name clarifies our offerings and makes them easier for you to navigate — one website, one team, one trusted partner.